Pilot Plants, Lab-Scale & R&D Units
Kerone’s Pilot Plants, Lab-Scale & R&D Units provide the essential bridge between laboratory-scale discovery and full-scale commercial production.
Engineered precision for Pilot Plants, Lab-Scale & R&D Units.
Kerone’s Pilot Plants, Lab-Scale & R&D Units provide the essential bridge between laboratory-scale discovery and full-scale commercial production. These compact, flexible, and precisely instrumented systems allow researchers, process engineers, and product developers to validate process parameters, test new formulations, and optimize production recipes before committing to large-scale capital investment.
Kerone designs its pilot and R&D units to be functionally equivalent to their industrial-scale counterparts, ensuring that results obtained at pilot scale are reliably scalable. With modular construction and comprehensive data acquisition systems, these units accelerate product development cycles and reduce scale-up risk across all industries.
Our advanced AI, ML, and IoT technologies, this solution delivers smarter automation, real-time insights, and predictive intelligence to enhance efficiency and drive future-ready growth.
Continuous tracking of process parameters with instant adjustments.
Intelligent fault detection to prevent failures before they occur.
Dynamic tuning of operations for maximum output and efficiency.
The thermodynamic architecture of our Pilot Plants, Lab-Scale & R&D Units incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
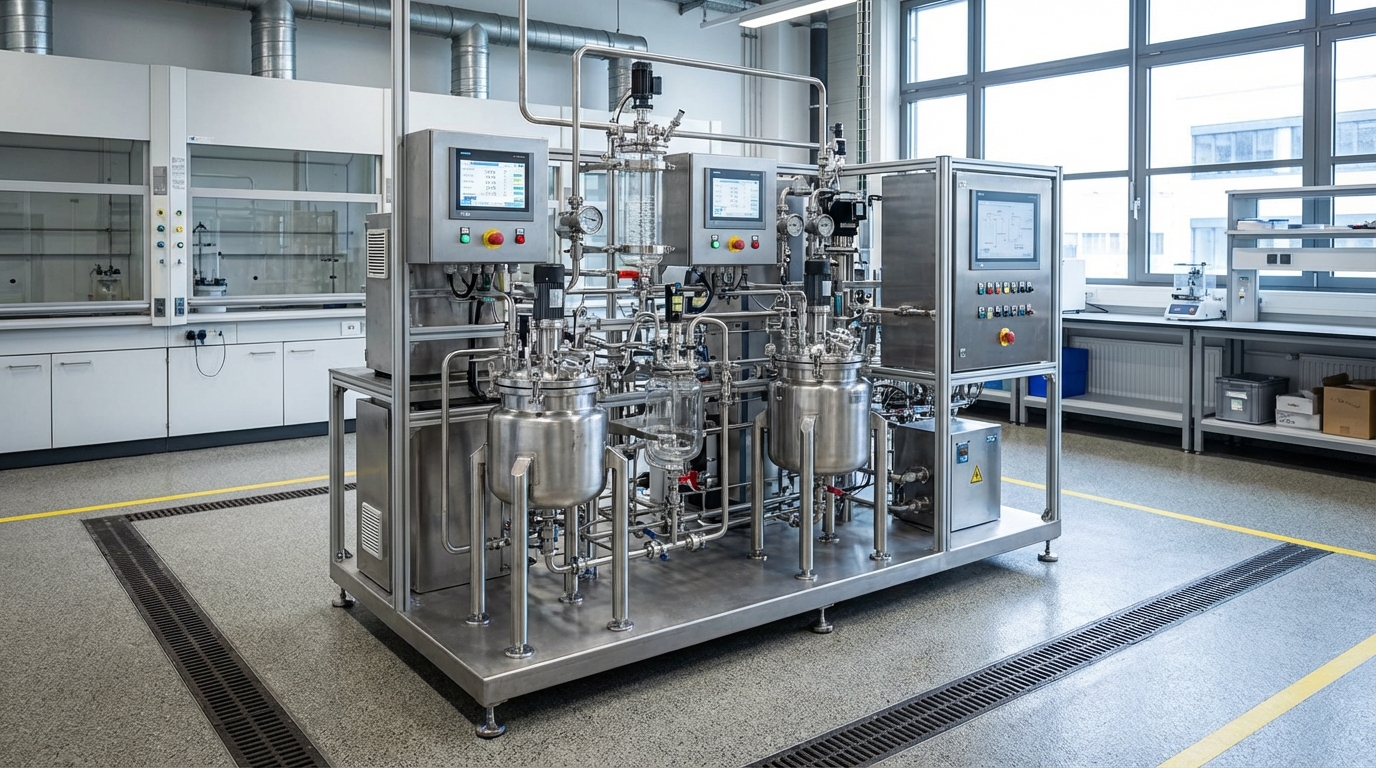
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Pilot Plants, Lab-Scale & R&D Units. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).
Pilot Plants, Lab-Scale & R&D Units
Click to view high-res
Pilot Plants, Lab-Scale & R&D Units
Click to view high-res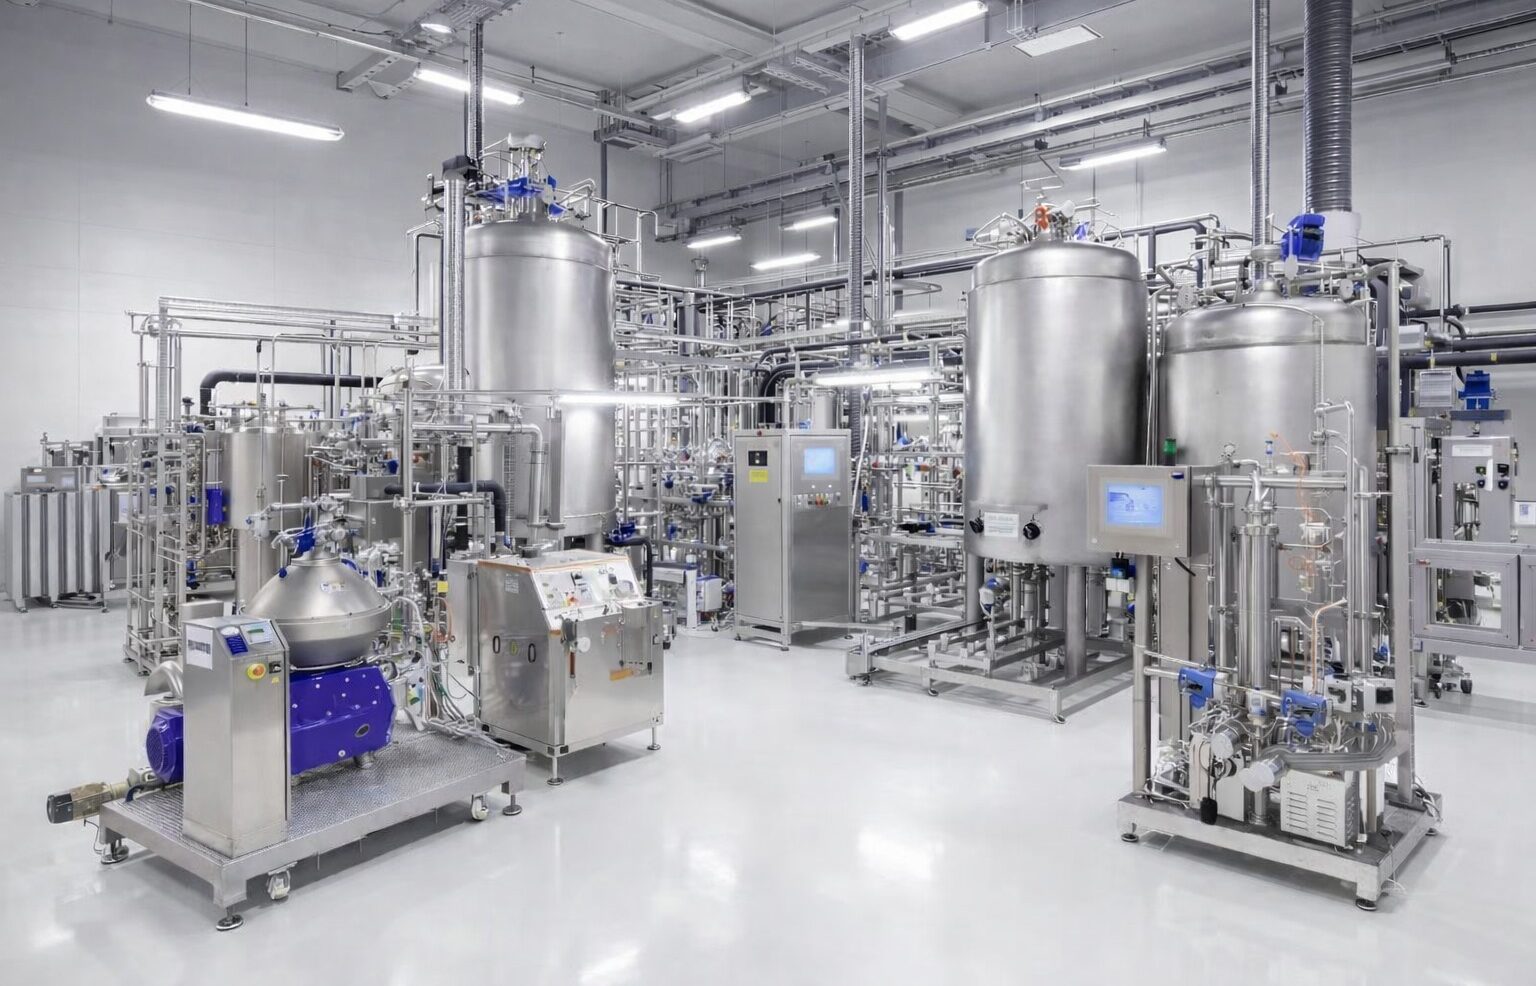
Pilot Plants, Lab-Scale & R&D Units
Click to view high-res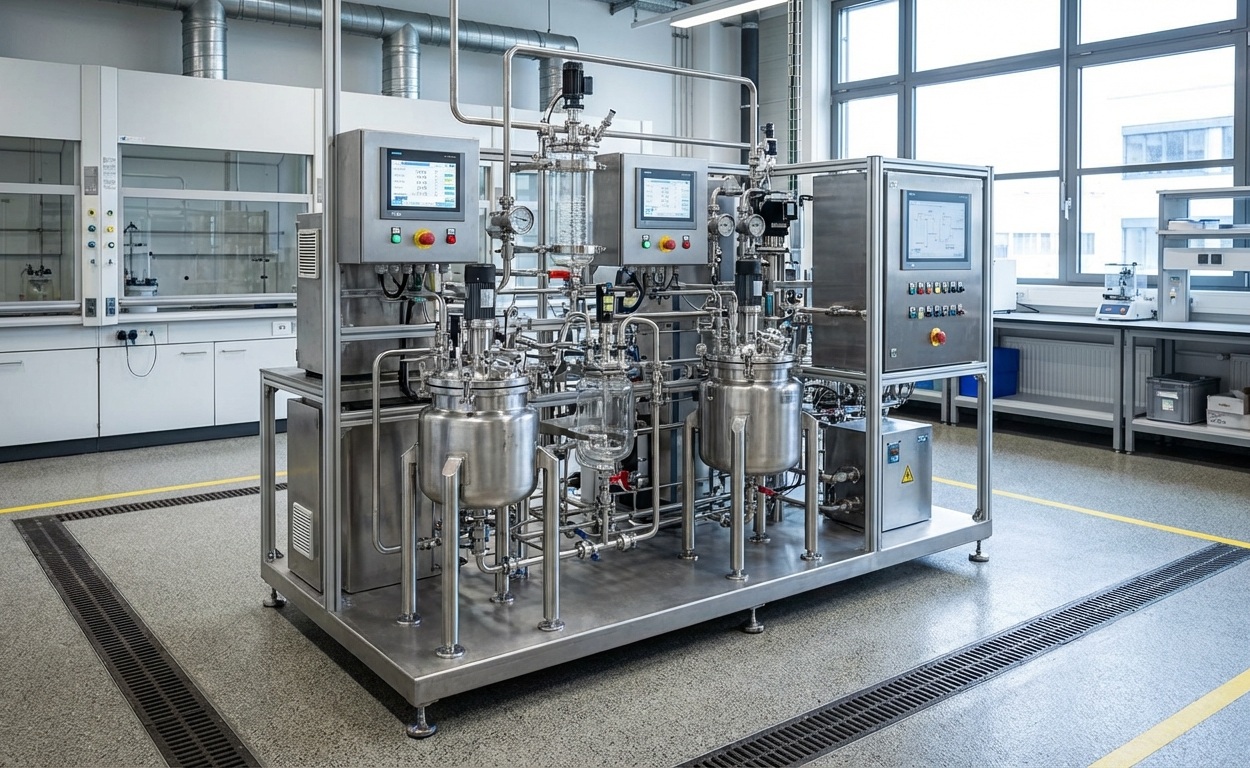
Pilot Plants, Lab-Scale & R&D Units
Click to view high-res
Pilot Plants, Lab-Scale & R&D Units
Click to view high-res
Pilot Plants, Lab-Scale & R&D Units
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
Reliable Scale-up Correlation
Functionally equivalent design to full-scale systems for reliable scale-up correlation
Detailed Experimental Analysis
High-resolution data acquisition and process visualization for detailed experimental analysis
Diverse Experimental Programs
Flexible and reconfigurable process configurations to support diverse experimental programs
GLP/GMP Compliant Construction
GLP/GMP compliant construction for pharmaceutical and food R&D applications
Compact Footprint
Compact footprint for lab and pilot facility integration without major civil works
Safe Operation
Safe operation with comprehensive interlock systems and operator protection measures
Wide Range of Process Parameter
Wide range of process parameter control including temperature, pressure, flow, and composition
Easy Cleaning and Changeover Design
Easy cleaning and changeover design to support multi-product and multi-formulation testing
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Pharmaceutical API and formulation ...
Pharmaceutical API and formulation process development and optimization studies
Food ingredient processing trials f...
Food ingredient processing trials for new product development and shelf-life validation
Chemical reaction kinetics studies ...
Chemical reaction kinetics studies and catalyst screening using bench-top reactors
Biochar and biomass conversion proc...
Biochar and biomass conversion process optimization at pilot scale
Coating and surface treatment proce...
Coating and surface treatment process parameter development for new substrates
Drying and thermal processing devel...
Drying and thermal processing development for novel materials with unknown properties
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
Beyond pharmaceutical and food product development, pilot and R&D units are widely used in chemical process engineering for reaction kinetics studies and catalyst screening, biochar and biomass conversion research for optimizing pyrolysis and carbonization parameters before full-scale plant investment, coating and surface treatment development when qualifying new substrate-coating combinations, and advanced materials research where novel formulations need controlled small-scale validation before scale-up. Renewable energy technology developers use pilot gasification and biomass conversion units to validate feedstock behavior before committing to commercial-scale system design. Specialty chemical and polymer producers use pilot reactors to optimize new formulations under realistic process conditions. Any industry developing a new thermal, chemical, or biological process benefits from pilot-scale validation, since the cost of discovering a process limitation at pilot scale is a small fraction of discovering it after full-scale commissioning.
Kerone typically provides operator training covering equipment operation, safety interlocks, and data acquisition system use, along with process development support to help the research team establish baseline operating parameters for their specific application. Documentation includes equipment manuals, P&ID drawings, and calibration certificates for installed instrumentation. For GMP-compliant units, IQ/OQ/PQ validation support helps the client's quality team establish the documentation trail required for regulatory submissions. Ongoing technical support is available for troubleshooting process issues that arise during the experimental phase, since pilot work often surfaces questions that weren't anticipated during initial commissioning. Kerone's own R&D center also offers contract pilot trial services for companies that want to validate a process before committing to purchasing dedicated pilot equipment of their own.
Kerone's pilot and lab units are built with modular process sections and reconfigurable parameter ranges specifically so a single piece of equipment can support testing across different formulations, feedstocks, or product variants without requiring separate dedicated equipment for each. Removable process modules, adjustable temperature and pressure ranges, and flexible material handling fixtures allow the same core unit to run trials on, for example, multiple powder formulations or biomass feedstock types in sequence. Validated cleaning protocols between trials prevent cross-contamination when switching between formulations, which is particularly important for pharmaceutical and food-grade applications. This flexibility is valuable for research organizations running a continuous pipeline of different product trials, since it avoids the capital cost of separate equipment for every formulation under development while still generating scale-up-relevant data for each.
Scale-up typically follows a staged approach: pilot data establishes the validated process window, including optimal temperature, residence time, and other critical parameters, after which the commercial equipment is designed to replicate the same dimensionless relationships at full throughput. Kerone's engineering team uses the pilot data to size heat exchangers, reactor volumes, and material handling capacity for the commercial system, validating that scale-up correlations hold before finalizing the full design. A demonstration or pre-commercial run at an intermediate scale is sometimes warranted for processes with significant scale-sensitive behavior, particularly in solids handling or mixing-dependent reactions. Throughout this process, retaining the original pilot equipment for ongoing formulation development and troubleshooting after commercial launch is common practice, since production-scale equipment isn't well suited for the frequent reconfiguration that ongoing R&D requires.
Building in-house pilot capability makes sense for organizations running continuous, high-frequency R&D programs where dedicated equipment availability and confidentiality outweigh the capital cost of ownership. Partnering with an external provider's pilot facility, such as Kerone's own R&D center, suits companies running occasional trials, validating a single new process before a capital decision, or lacking the technical staff to operate specialized pilot equipment safely and effectively. External partnership also provides access to a broader range of process technologies than most companies would justify purchasing for occasional use. Many organizations use a hybrid approach, maintaining basic lab-scale equipment in-house for routine formulation work while using external pilot facilities for less frequent, larger-scale validation trials that would otherwise sit idle most of the year if purchased outright.
Pilot-scale data is reliable for scale-up prediction only when the pilot unit preserves the key dimensionless ratios and process dynamics that govern the specific process, such as residence time distribution, heat and mass transfer coefficients, and mixing patterns relevant to the application. Kerone designs pilot units to be functionally and geometrically representative of the full-scale equivalent rather than simply a smaller version with different proportions, which is what makes the resulting data trustworthy for scale-up decisions. A common misconception is that any reduction in scale preserves these relationships automatically, when in practice naive scale-down can distort critical parameters like surface-area-to-volume ratio in ways that make the data misleading. Buyers should ask specifically how scale-up correlation has been validated for their process type before relying on pilot results for capital investment decisions.
A frequent mistake is selecting a pilot unit that is too small or too simplified relative to the intended full-scale process, which produces data that does not scale reliably because key geometric or flow ratios differ between the pilot and the eventual commercial system. Companies sometimes skip pilot trials entirely under time pressure and move straight to a full commercial build, only to discover process issues at a much higher cost once production scale equipment is already installed. Another common error is underestimating the instrumentation needed to capture useful data, building a pilot unit with manual controls and minimal logging that cannot generate the statistically meaningful dataset required for confident scale-up decisions. Engaging a partner experienced in scale-up correlation, rather than treating the pilot unit as a smaller, cheaper version of the final system, avoids most of these issues.
Kerone's pilot units range from lab-scale units processing grams per hour up to pilot-scale systems handling several hundred kilograms per hour, depending on the process type.
Yes, Kerone designs pilot systems with dimensionally equivalent geometry and process dynamics to ensure that scale-up correlations are reliable and valid.
Yes, Kerone offers GMP-compliant pilot plants with full documentation, material certification, IQ/OQ/PQ validation support, and audit trail capabilities.
Many Kerone pilot units feature modular process sections that can be rearranged or replaced to accommodate different process configurations and experimental programs.
Yes, Kerone provides pilot testing services at its own facilities and also offers rental options for clients who need temporary access to specific processing technologies.
Kerone integrates multi-channel data loggers, real-time visualization dashboards, and exportable data formats including CSV and OPC-UA for process analysis.
Delivery time for custom pilot plants typically ranges from 6 to 14 weeks depending on complexity, customization requirements, and component availability.
Yes, Kerone designs pilot units in both batch and continuous configurations, and some units support switchable operation between both modes for maximum experimental flexibility.
Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.