Freeze Dryer
Kerone brings over 50 years of experience in designing high-performance freeze dryer for a wide range of industrial and commercial applications.
Engineered precision for Freeze Dryer.
Kerone brings over 50 years of experience in designing high-performance freeze dryer for a wide range of industrial and commercial applications. Built with advanced heat transfer mechanisms and automated controls, Kerone’s freeze dryer are engineered to deliver optimal drying performance while maintaining product integrity.
Kerone Freeze Dryers are designed to handle the lyophilization needs of research and pilot plant laboratories.
At Kerone, we produce freeze dryers that can be fall in various range based on the complexity of design from simple to very complex, all depends on the fluid or slurries under processing. The difference in the designs rare the in atomization, pattern of airstream, air heating systems/technique, and separation and collection unit.
The drying process is as follows: Firstly, the internal moisture of food has been frozen in the low-temperature environment. Secondly, in drying step, the ice inside previous raw material will directly be converted into steam evaporation during a near-vacuum environment.
Finally, the internal moisture of food will dramatically decrease. The whole dewatering process is under a lower temperature environment than that of traditional dryer.
Our advanced AI, ML, and IoT technologies, this solution delivers smarter automation, real-time insights, and predictive intelligence to enhance efficiency and drive future-ready growth.
The thermodynamic architecture of our Freeze Dryer incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
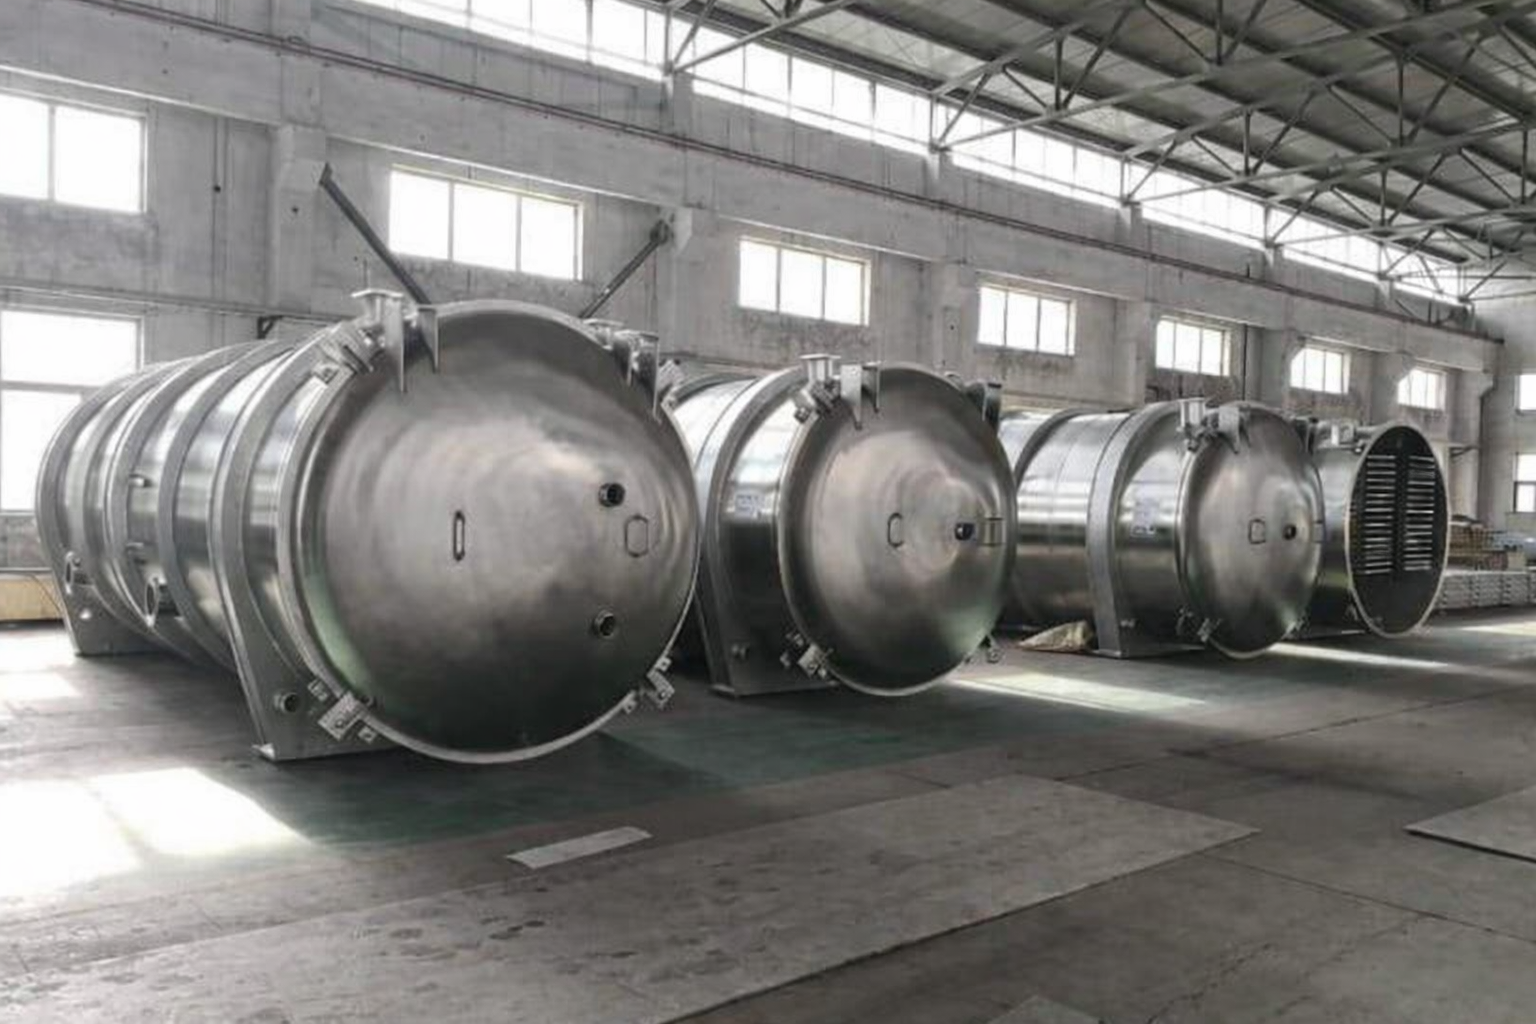
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Freeze Dryer. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).
Freeze Dryer
Click to view high-res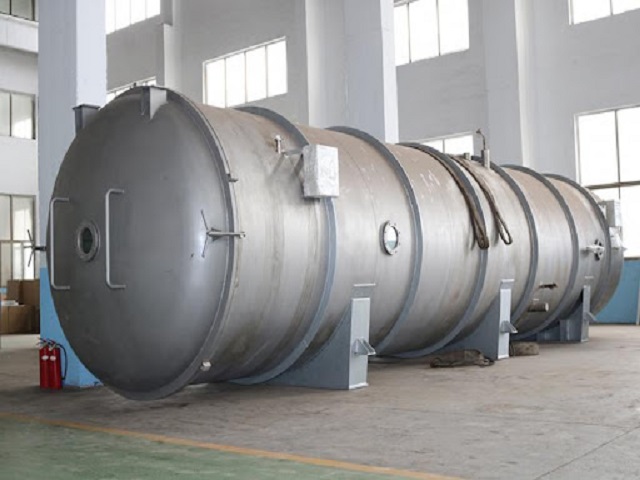
Freeze Dryer
Click to view high-res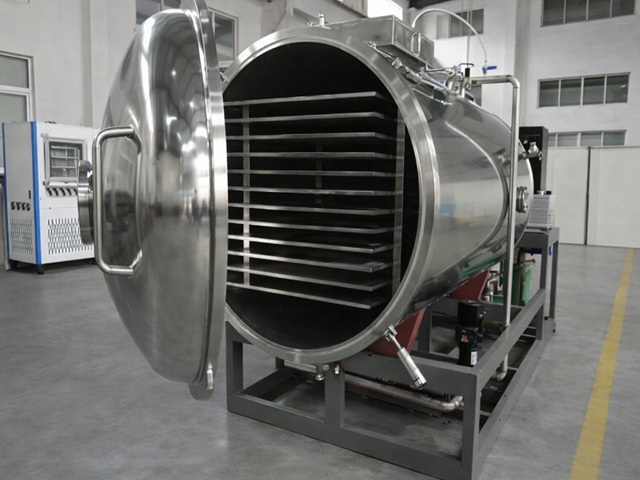
Freeze Dryer
Click to view high-res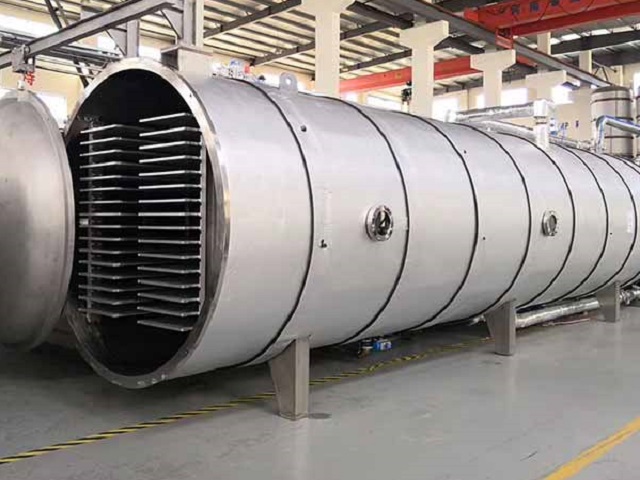
Freeze Dryer
Click to view high-res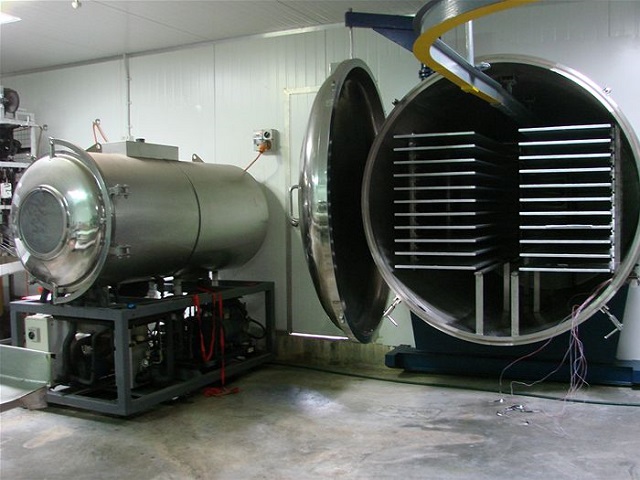
Freeze Dryer
Click to view high-res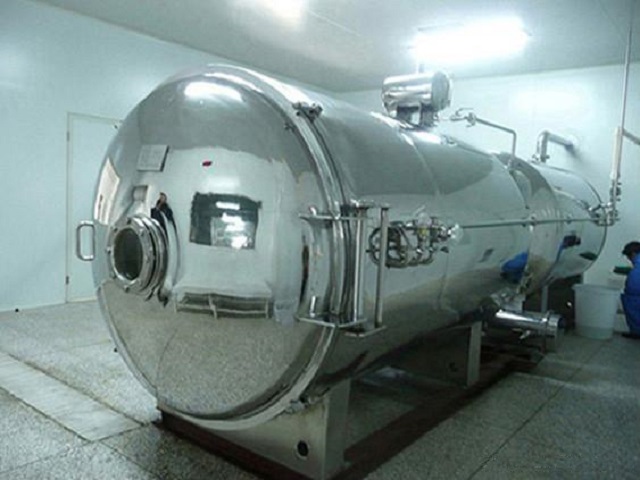
Freeze Dryer
Click to view high-res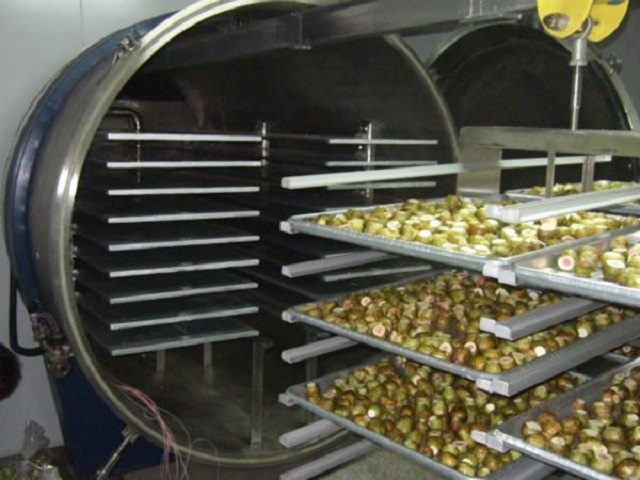
Freeze Dryer
Click to view high-res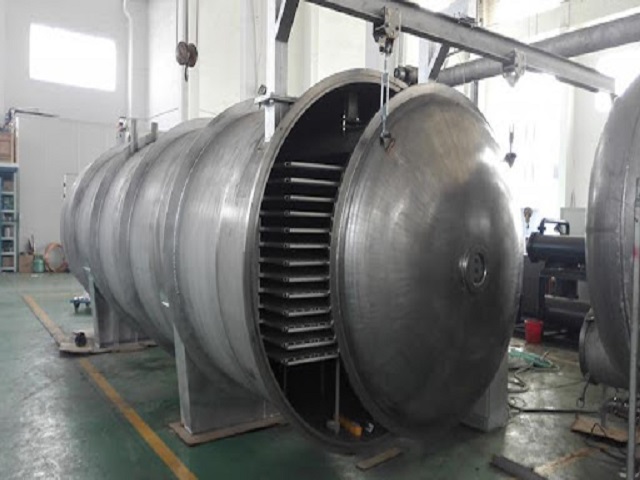
Freeze Dryer
Click to view high-res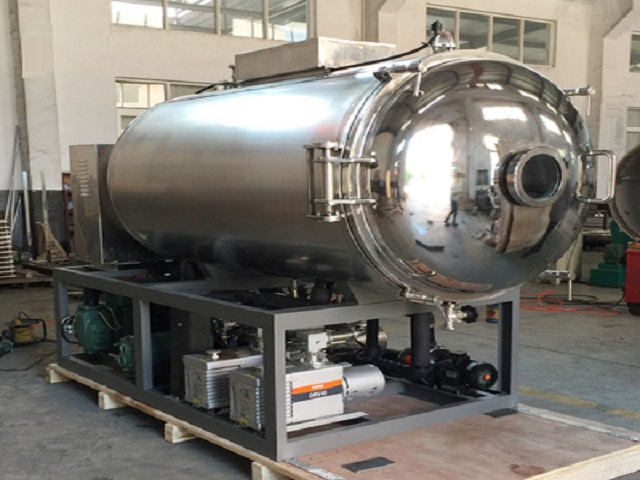
Freeze Dryer
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
Energy-efficient Design
Energy-efficient design with advanced heat management.
Uniform Drying
Uniform drying with consistent temperature distribution.
Customizable Airflow and Heating
Customizable airflow and heating configurations.
Automatic Control Systems
Automatic control systems for precision and safety.
Robust Construction Ensuring
Robust construction ensuring long operational life.
Low Maintenance
Low maintenance with easy-to-clean components.
Ideal for Both Batch and
Ideal for both batch and continuous drying processes.
Optimized
Optimized for sensitive and bulk materials alike.
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Food & Beverage
Drying fruits, vegetables, meat, fish, and herbs.
Agriculture
Moisture removal from grains, seeds, and crops.
Pharmaceutical
Drying herbal extracts, granules, and powders.
Chemical & Mineral
Processing catalysts, pigments, and minerals.
Industrial
Drying of ceramics, coal, polymers, and composites.
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
A freeze dryer is an industrial system that removes moisture from materials using controlled heat and airflow.
It operates by circulating hot air or transferring heat to evaporate moisture from products efficiently.
It ensures faster drying, energy efficiency, and product uniformity.
Industries like food, agriculture, pharmaceutical, and chemical commonly use these dryers.
Yes, Kerone designs every system according to specific industry and process needs.
Yes, precise temperature control ensures safe drying for sensitive materials.
Kerone’s designs optimize heat recovery and minimize energy consumption.
Regular inspection, cleaning, and calibration ensure optimal performance and longer lifespan.
Yes, this is the primary reason pharmaceutical and biological products are freeze dried; the absence of heat and liquid water during lyophilization prevents the degradation reactions that would reduce potency in thermally dried or liquid-stored products.
Properly lyophilized products reconstitute rapidly in water due to the highly porous, sponge-like structure created by sublimation; reconstitution times of seconds to minutes are achievable for pharmaceutical vials.
Conventional heat-based drying exposes a product to elevated temperatures and, in many cases, a liquid water phase during evaporation, both of which can trigger degradation reactions in heat- or hydrolysis-sensitive compounds such as certain proteins, enzymes, and biological actives. Freeze drying avoids both of these stressors: the product remains frozen and solid during the critical primary drying stage, and moisture leaves as vapor through sublimation rather than passing through a liquid state. This combination of low temperature and avoidance of liquid water is precisely why freeze drying is the preferred method for pharmaceutical biologics, certain food actives, and other products where potency or structural integrity must be preserved through the drying process.
AISI 304 stainless steel offers strong corrosion resistance and is widely accepted across food and pharmaceutical regulatory frameworks for direct product contact, which matters significantly in freeze drying applications given the sensitive, often high-value nature of the materials being processed â biological actives, pharmaceutical intermediates, and premium food products. The chamber, trays, and vapor condenser are all surfaces that contact either the product directly or the water vapor removed from it, so material consistency across all these components reduces contamination risk and simplifies cleaning validation. This material choice also supports the repeated cleaning and sterilization cycles that pharmaceutical-grade freeze drying operations typically require between batches.
The vacuum system is what enables sublimation to occur at low temperature by reducing chamber pressure below the point where ice can exist as a stable solid at typical primary drying temperatures. A high-performance vacuum system maintains the deep vacuum needed consistently throughout the drying cycle, which directly affects how quickly sublimation proceeds â weaker or unstable vacuum performance extends cycle time and can risk partial product melting if pressure rises above the critical point for the product's formulation. Kerone pairs the vacuum system with the refrigeration system's condenser capacity, since the condenser must continuously capture sublimated vapor to maintain the vacuum level the process requires throughout the full cycle.
Many freeze-dried products, particularly pharmaceutical and certain food actives, require packaging under vacuum or inert gas immediately after drying to prevent moisture reabsorption or oxidative degradation before the product reaches its final sealed container. Kerone's freeze dryers support a wide range of product containers with provision for sealing under vacuum or inert gas directly as part of the drying cycle, which avoids the quality risk of exposing a freshly dried, highly hygroscopic product to ambient air during a separate packaging step. Buyers whose products are sensitive to moisture reabsorption or oxygen exposure should specify this sealing requirement early, since it affects chamber and tray configuration.
Sublimation during freeze drying leaves behind a highly porous, sponge-like internal structure where ice crystals once occupied space, and this porosity is precisely what allows water to rapidly re-penetrate the dried material during reconstitution. Properly executed freeze drying typically achieves reconstitution times of seconds to minutes for pharmaceutical vials, and slow or incomplete reconstitution can indicate that the original drying cycle didn't achieve adequate porosity, possibly due to incomplete sublimation or structural collapse during the process. This is why reconstitution performance is often used as a downstream quality check that reflects how well the freeze drying cycle itself was executed, beyond just confirming the product reached its target moisture level.

Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.