Food & Nutraceutical Processing Plants
Kerone’s Food & Nutraceutical Processing Plants are purpose-built solutions for the safe, hygienic, and efficient transformation of raw food materials and botanical ingredients into high-quality consumer products and health supplements.
Engineered precision for Food & Nutraceutical Processing Plants.
Kerone’s Food & Nutraceutical Processing Plants are purpose-built solutions for the safe, hygienic, and efficient transformation of raw food materials and botanical ingredients into high-quality consumer products and health supplements. From raw ingredient preparation, extraction, concentration, and drying to blending, encapsulation, and packaging, Kerone designs integrated food and nutraceutical processing lines that adhere to the highest standards of food safety, GMP compliance, and nutritional integrity. Whether it’s a spray-dried herbal extract, a freeze-dried probiotic supplement, or a thermally processed ready meal, Kerone brings deep domain expertise to every stage of the production process.
Our advanced AI, ML, and IoT technologies, this solution delivers smarter automation, real-time insights, and predictive intelligence to enhance efficiency and drive future-ready growth.
Continuous tracking of process parameters with instant adjustments.
Intelligent fault detection to prevent failures before they occur.
Dynamic tuning of operations for maximum output and efficiency.
The thermodynamic architecture of our Food & Nutraceutical Processing Plants incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Food & Nutraceutical Processing Plants. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).

Food & Nutraceutical Processing Plants
Click to view high-res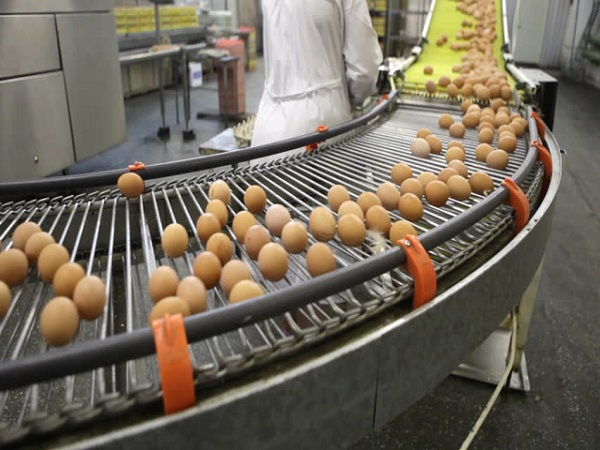
Food & Nutraceutical Processing Plants
Click to view high-res
Food & Nutraceutical Processing Plants
Click to view high-res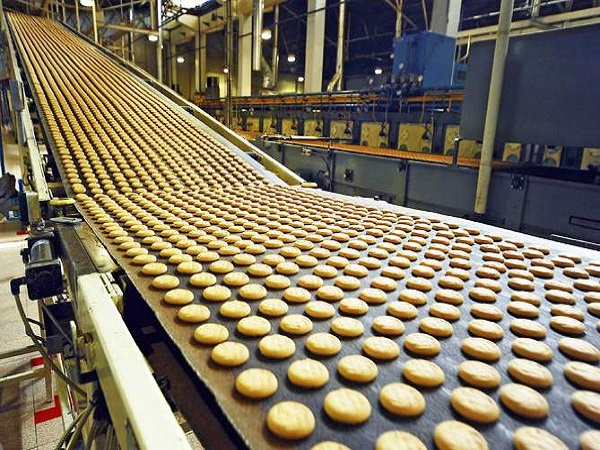
Food & Nutraceutical Processing Plants
Click to view high-res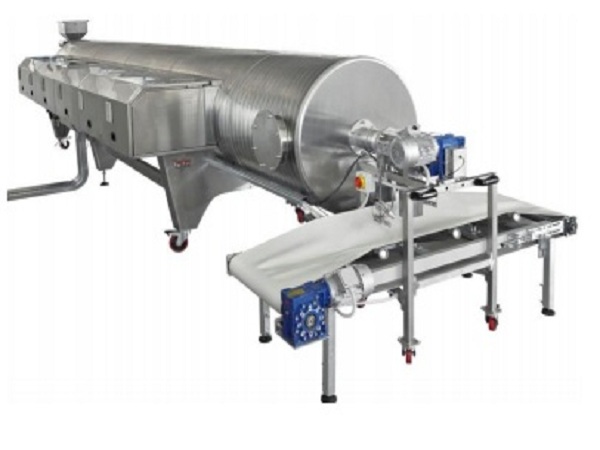
Food & Nutraceutical Processing Plants
Click to view high-res
Food & Nutraceutical Processing Plants
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
Full Documentation Support
GMP and FSSC 22000 compliant plant design with full documentation support
Hygienic SS 316L Construction
Hygienic SS 316L construction with electropolished interiors and sanitary fittings
CIP and SIP Systems
CIP and SIP systems for efficient, validated in-place cleaning and sterilization
Gentle Processing Technologies
Gentle processing technologies to preserve nutritional value, bioactivity, and color
Heat-sensitive Ingredients
Cold processing and low-temperature vacuum evaporation options for heat-sensitive ingredients
Integrated Quality Control Systems
Integrated quality control systems with in-line NIR, pH, and moisture measurement
Full Traceability and Batch
Full traceability and batch record management through MES/ERP integration
Full Commercial Production Lines
Scalable designs from pilot-scale R&D units to full commercial production lines
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Herbal and botanical extract concen...
Herbal and botanical extract concentration and spray drying for supplement manufacturing
Probiotic culture drying and encaps...
Probiotic culture drying and encapsulation for stability and shelf-life enhancement
Fruit and vegetable juice concentra...
Fruit and vegetable juice concentration, pasteurization, and aseptic processing
Protein powder processing including...
Protein powder processing including whey, soy, and plant-based protein isolation and drying
Vitamin and mineral premix blending...
Vitamin and mineral premix blending and granulation for tablet and capsule production
Ready meal and convenience food the...
Ready meal and convenience food thermal processing, retort, and packaging lines
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
Kerone's plants are designed to comply with FSSC 22000, FDA 21 CFR Parts 110 and 111, EU GMP, EHEDG hygienic design standards, and local food safety regulations.
Yes, Kerone designs processing lines for both liquid (juices, extracts, emulsions) and solid (powders, granules, tablets, capsules) food and nutraceutical products.
Yes, Kerone offers low-temperature processing options including vacuum evaporation, freeze drying, and spray drying at controlled temperatures to preserve bioactive compounds.
Yes, precise temperature control ensures safe drying for sensitive materials.
Kerone integrates validated CIP (Clean-in-Place) and SIP (Sterilize-in-Place) systems designed to FDA and EHEDG standards, ensuring efficient, reproducible cleaning cycles.
Yes, Kerone provides aqueous extraction, alcohol extraction, and supercritical CO2 extraction systems for botanical, herbal, and marine ingredient processing.
Kerone designs both batch and continuous processing configurations depending on production volume, product variety, and flexibility requirements.
Kerone integrates MES and ERP systems that capture batch records, raw material lot numbers, process parameters, and quality data for full end-to-end traceability.
Kerone's plants support production of powders, granules, tablets, soft gels, hard capsules, effervescent tablets, sachets, and liquid nutraceutical formats.
Food and nutraceutical products require drying systems that preserve flavor, color, nutrients, and bioactive compounds while meeting strict hygiene and regulatory standards. Kerone offers spray dryers, freeze dryers, tray dryers, and microwave drying systems specifically designed for food-grade applications with SS304/316 construction, CIP-compatible designs, and FDA/GMP compliance. Spray drying is ideal for liquid formulations, while freeze drying is the gold standard for preserving heat-sensitive bioactives such as probiotics and herbal extracts.
For food processing, the best microwave drying systems combine microwave energy with controlled airflow to balance rapid drying with product quality preservation. Kerone's food-grade microwave dryers feature stainless steel construction, hygienic design with no dead spots, CIP compatibility, and precise power modulation. They are ideal for snacks, nuts, spices, herbs, seafood, ready-to-eat meals, and instant food products. Kerone's systems are available in continuous conveyor and tunnel configurations for high-throughput operations and in batch chamber designs for smaller productions or R&D.
Food and beverage drying requires equipment that maintains product safety (HACCP compliance), preserves sensory and nutritional quality, and meets food-contact material standards (FDA, EU 10/2011). Kerone supplies spray dryers for milk powder, juices, and instant beverages; belt dryers for fruits, vegetables, and seafood; rotary dryers for sugar and salt; and freeze dryers for premium products. Hygienic design principles, including sloped surfaces, crevice-free welding, and quick-release clamps, minimize contamination risk and simplify cleaning validation.
Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.