Microwave Sterilisation
Microwave sterilization is a process of using microwave energy to kill microorganisms and pathogens on a variety of surfaces and objects.
Engineered precision for Microwave Sterilisation.
Microwave sterilization is a process of using microwave energy to kill microorganisms and pathogens on a variety of surfaces and objects. This method is commonly used in the food industry to sterilize and extend the shelf life of various food products.
The process of microwave sterilization involves exposing the material to be sterilized to high-frequency electromagnetic radiation, typically at a frequency of 2450 MHz. The energy from the microwaves is absorbed by the water molecules in the material, causing them to heat up and ultimately kill any bacteria or other microorganisms present.
Microwave sterilization has several advantages over other methods of sterilization. It is a relatively fast process, with sterilization times typically ranging from a few seconds to a few minutes. It is also a dry process, which can be beneficial for materials that may be damaged by exposure to steam or other types of moisture.
Kerone’s microwave sterilization systems can be customized to meet the specific requirements of each application. They are designed for ease of operation and maintenance, featuring automated controls and real-time monitoring systems to ensure the safety, consistency, and effectiveness of the sterilization process.
Microwave sterilization can be a highly effective method for sterilizing certain types of materials and products. However, it is important to carefully evaluate the specific requirements of each application and follow appropriate safety guidelines to ensure optimal performance and reliable sterilization results.
The thermodynamic architecture of our Microwave Sterilisation incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
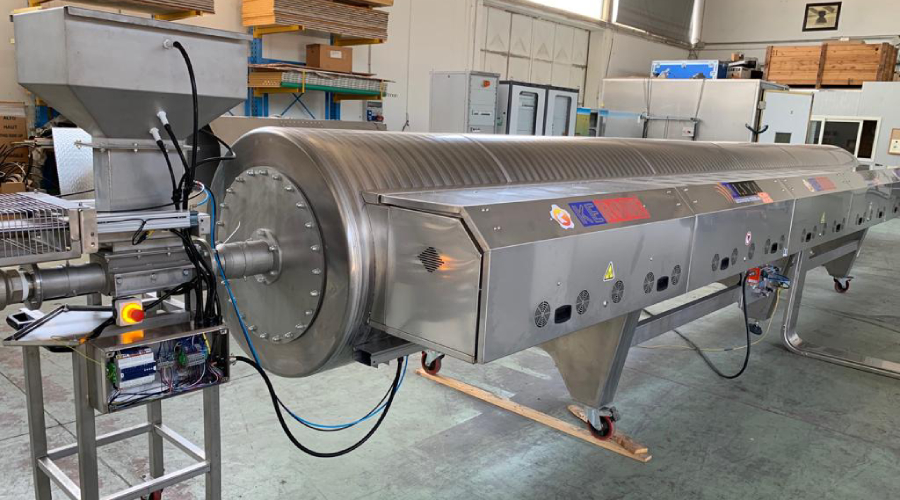
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Microwave Sterilisation. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).
Microwave Sterilisation
Click to view high-res
Microwave Sterilisation
Click to view high-res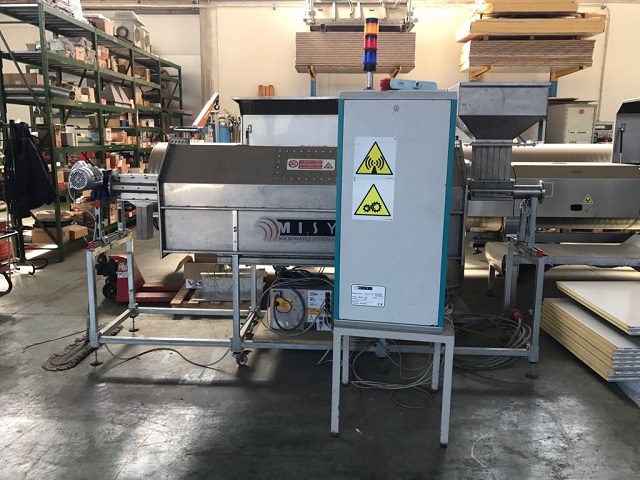
Microwave Sterilisation
Click to view high-res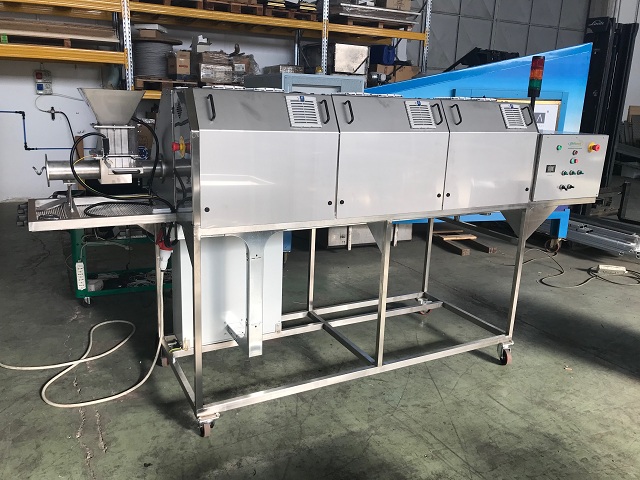
Microwave Sterilisation
Click to view high-res
Microwave Sterilisation
Click to view high-res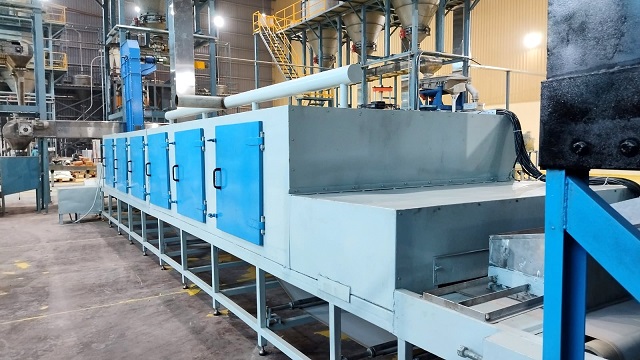
Microwave Sterilisation
Click to view high-res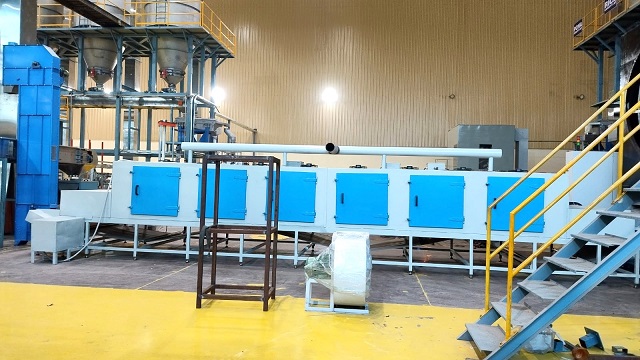
Microwave Sterilisation
Click to view high-res
Microwave Sterilisation
Click to view high-res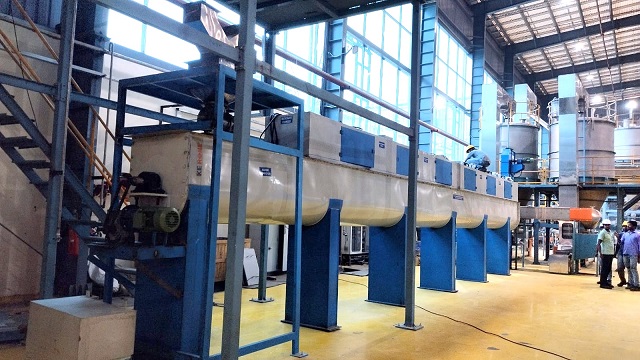
Microwave Sterilisation
Click to view high-res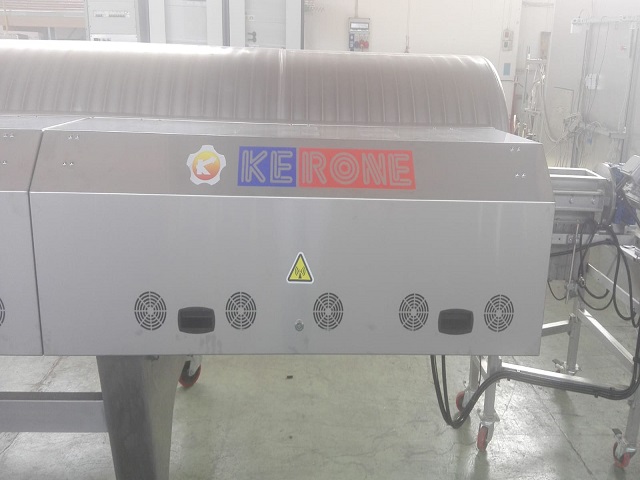
Microwave Sterilisation
Click to view high-res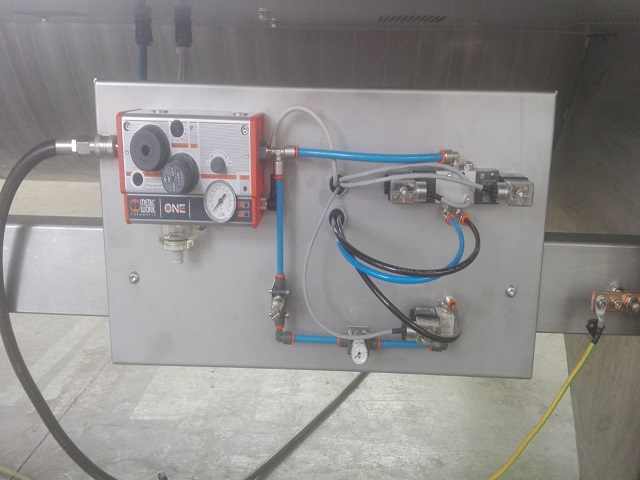
Microwave Sterilisation
Click to view high-res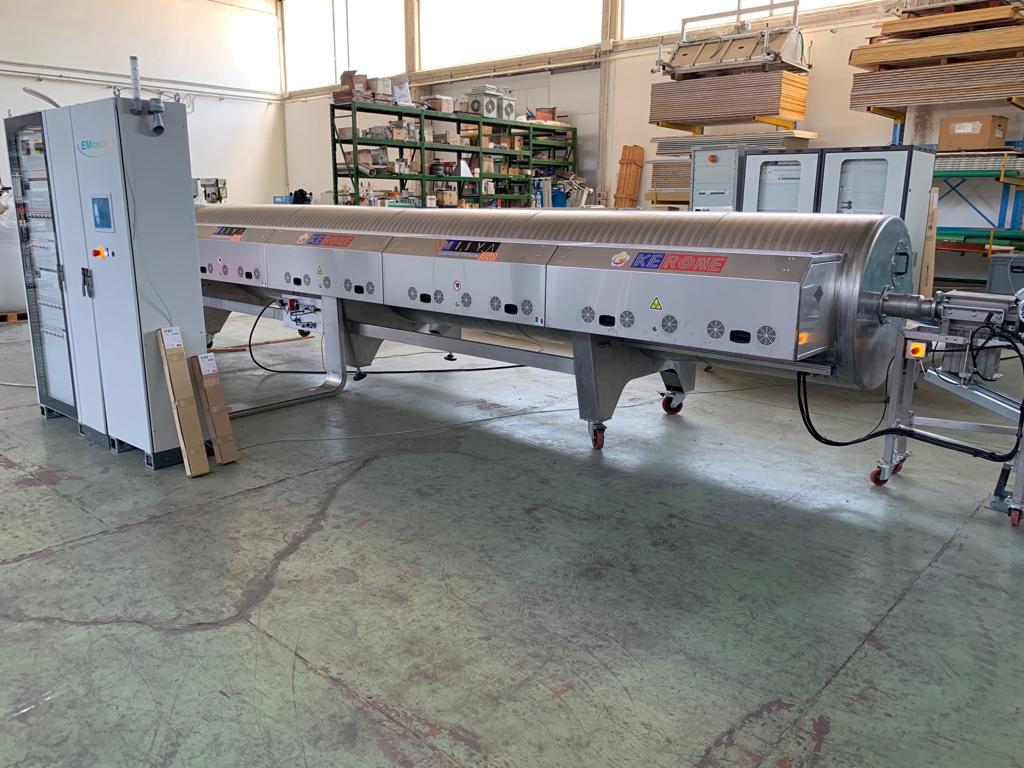
Microwave Sterilisation
Click to view high-res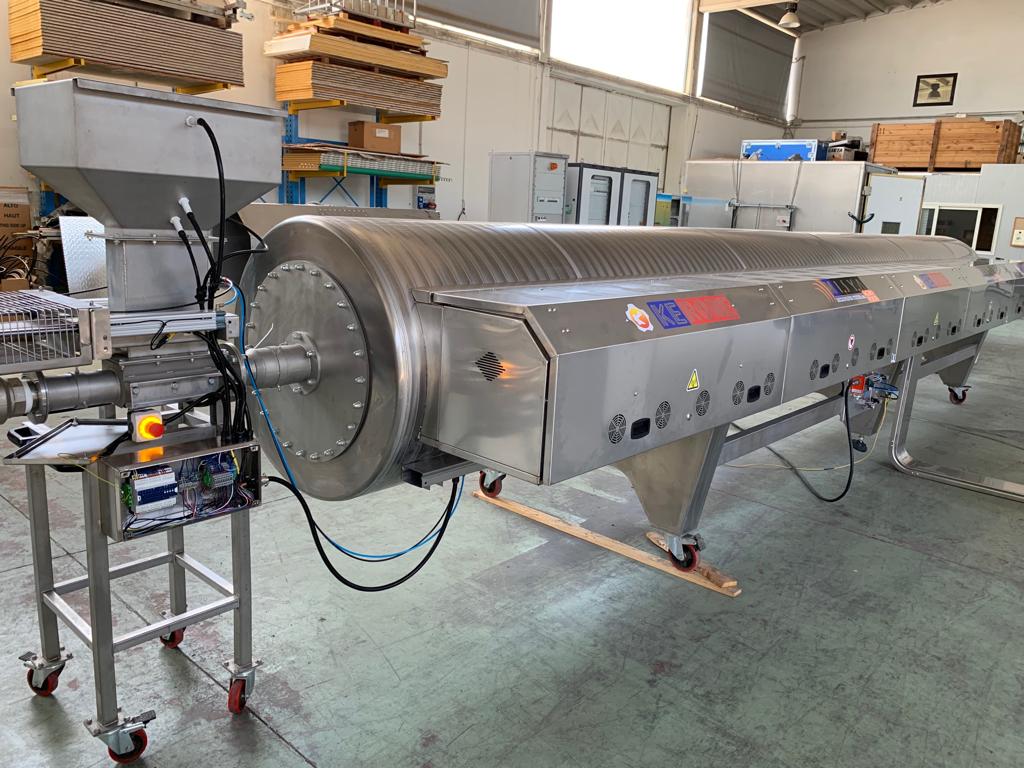
Microwave Sterilisation
Click to view high-res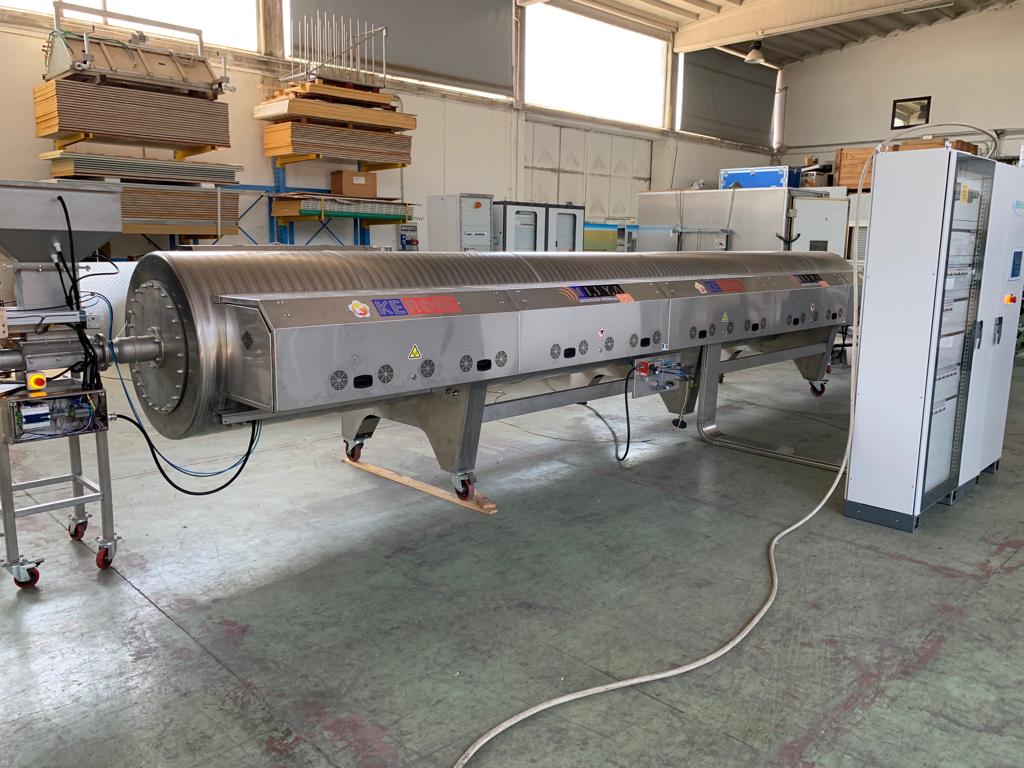
Microwave Sterilisation
Click to view high-res
Microwave Sterilisation
Click to view high-res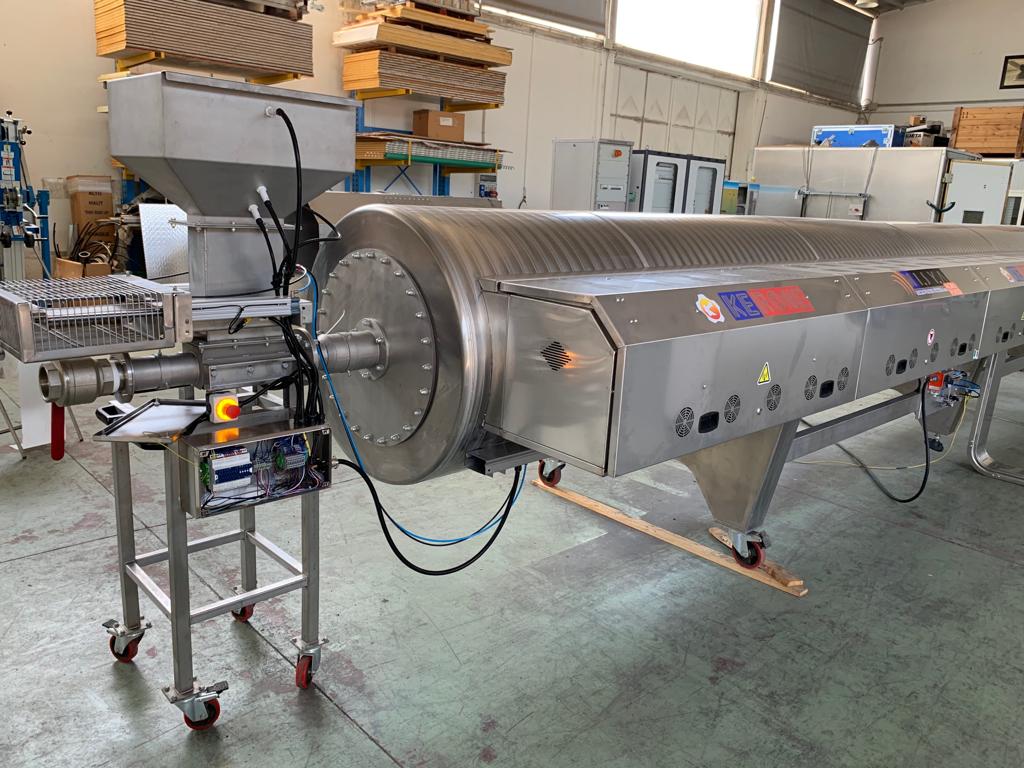
Microwave Sterilisation
Click to view high-res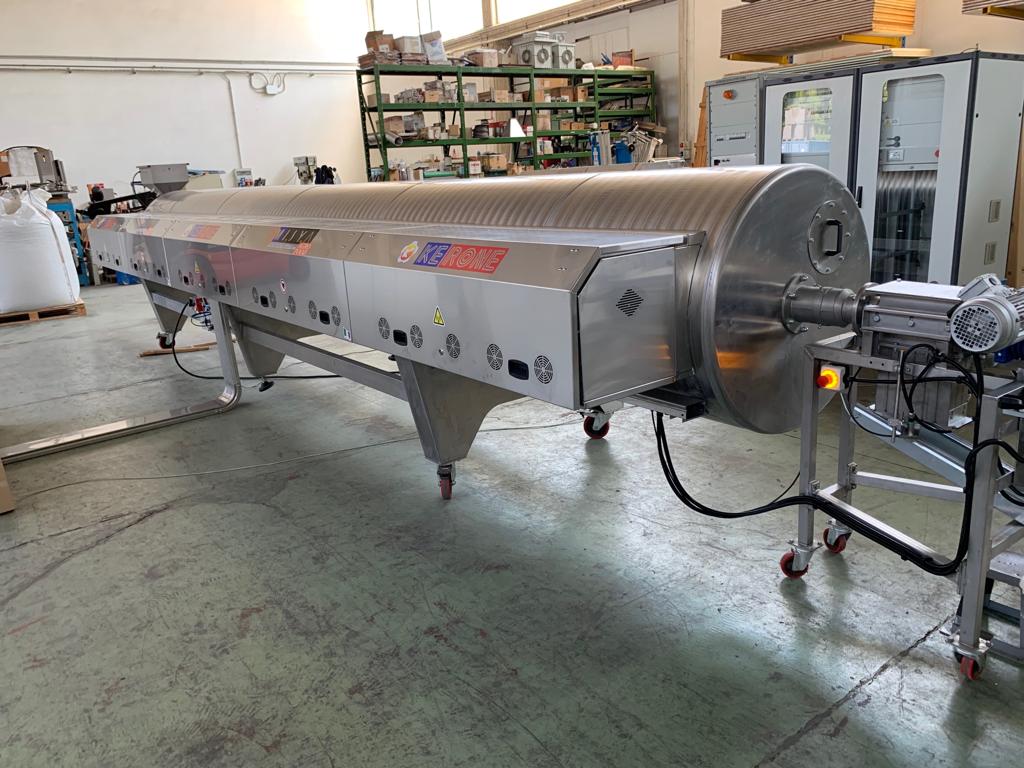
Microwave Sterilisation
Click to view high-res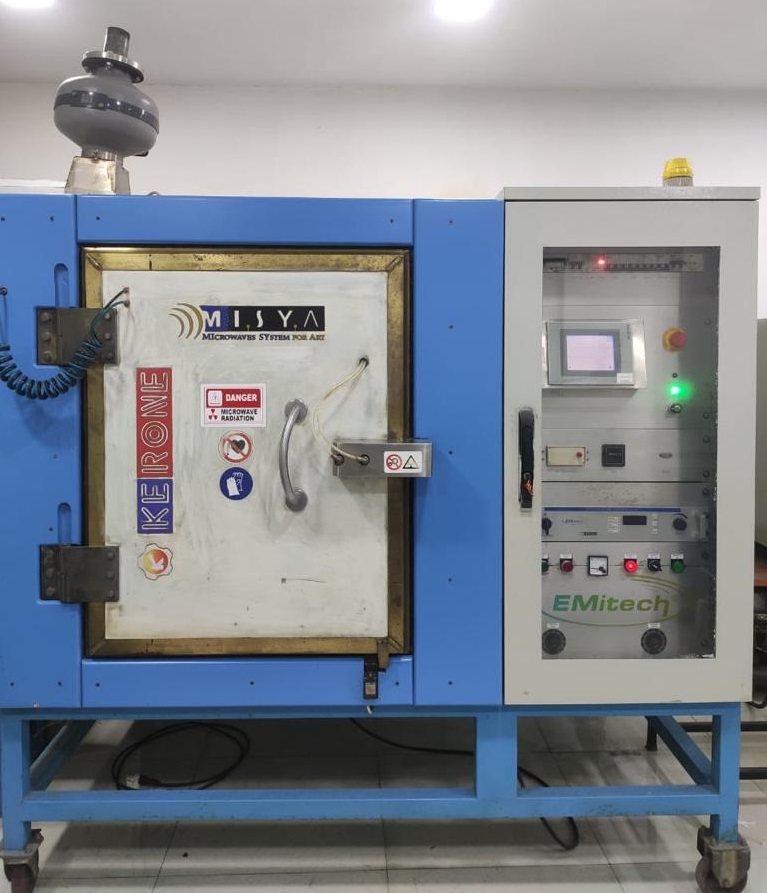
Microwave Sterilisation
Click to view high-res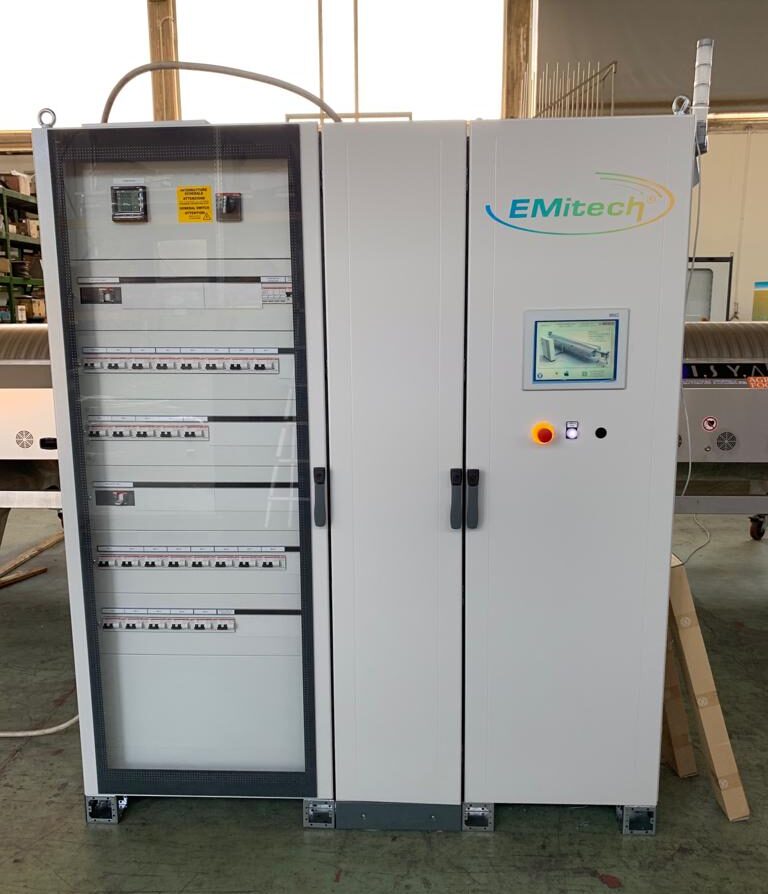
Microwave Sterilisation
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
High Thermal and Processing
High thermal and processing efficiency
Low Maintenance and Easy
Low maintenance and easy operation
Suitable
Suitable for heat-sensitive materials
Fully Adjustable and
Fully adjustable and customizable process parameters
Available in Batch and
Available in batch and continuous configurations
Uniform Processing and
Uniform processing and consistent product quality
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Food industry processing systems
Food industry processing systems
Chemical and polymer processing
Chemical and polymer processing
Pharmaceutical ingredients and inte...
Pharmaceutical ingredients and intermediates
Ready‑to‑eat (RTE) food production
Ready‑to‑eat (RTE) food production
Specialized heating, drying, or mat...
Specialized heating, drying, or material transformation processes
Industrial material modification an...
Industrial material modification and thermal treatment
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
Validation typically combines temperature mapping across the product load to confirm uniform heat distribution, microbial challenge studies using indicator organisms to demonstrate lethality, and F0 value calculations that quantify the equivalent sterilisation effect at a reference temperature. These steps generate the documented evidence regulators and quality auditors expect before a sterilisation process is approved for commercial use. Kerone supports this validation work directly, providing temperature profiling data and process documentation aligned with standard validation protocols used in food safety and pharmaceutical manufacturing. Buyers should request this validation support explicitly during the procurement process, since a sterilisation system without proper documentation cannot be deployed in regulated production environments regardless of its technical performance.
It is used for efficient processing, heating, drying or material transformation.
High efficiency, process reliability and complete customization.
Yes, Kerone offers fully customized engineering solutions.
Food, chemical, pharma, biomass, rubber, textile and more.
Kerone ensures high product quality through strict engineering standards, advanced testing procedures, and precision-controlled manufacturing systems.
Validation involves temperature mapping, microbial challenge studies, and F0 value calculations following standard validation protocols, with full documentation provided by Kerone.
Products with very low moisture content, highly reflective metallic packaging, or those containing components sensitive to microwave energy may require alternative sterilisation approaches.
Yes, Kerone's modular continuous tunnel systems can be integrated into existing processing and packaging lines with appropriate engineering modifications.
Steam-based sterilisation introduces moisture into the product or packaging, which then requires a separate drying stage before the product can be packaged or stored, adding time, energy, and equipment to the line. Microwave sterilisation heats the product directly through dielectric absorption without introducing external steam or moisture, so the material reaches sterilising temperature and returns to a dry, stable state without an additional drying phase. This is one of the more underappreciated cost advantages of the technology: removing an entire process step from the line reduces both capital equipment needs and total processing time per batch, which compounds significantly across high-volume production runs.
Materials with very low moisture content don't absorb microwave energy efficiently, since the heating mechanism relies primarily on water molecules responding to the electromagnetic field, making sterilisation slow or uneven for very dry products. Items packaged in highly reflective metallic materials can also cause arcing or uneven field distribution inside the chamber, creating both a safety risk and inconsistent sterilisation results. Products containing components sensitive to microwave energy, certain electronic assemblies or specific packaging films, may also need alternative methods entirely. Before specifying microwave sterilisation, buyers should share full product and packaging details with their equipment supplier so the dielectric behaviour can be assessed and an alternative process recommended if microwave energy isn't the right fit.
Kerone's modular continuous tunnel systems are designed for integration into established processing and packaging lines, though the exact timeline depends on factors like conveyor speed matching, available floor space, and any electrical or utility modifications needed at the installation site. Because the tunnel uses a continuous belt-fed design rather than a standalone batch chamber, it can often slot into an existing line layout with engineering adjustments rather than requiring a complete line rebuild. Kerone's engineering team typically conducts a site assessment before installation to confirm throughput compatibility and identify any line modifications needed, which keeps changeover downtime predictable rather than open-ended.
Yes, microwave sterilisation achieves microbial elimination through direct thermal energy rather than chemical agents like ethylene oxide or other sterilising compounds, which removes the need for chemical residue testing, off-gassing periods, and the environmental handling requirements that come with chemical sterilisation methods. This is particularly relevant for food processors and pharmaceutical manufacturers facing tightening restrictions on chemical sterilants in several markets. Eliminating chemical inputs also simplifies worker safety protocols and reduces the regulatory documentation burden tied to chemical handling and disposal. For companies under pressure to reduce chemical usage in their processes, microwave sterilisation offers a thermal alternative that still meets validated microbial reduction standards without introducing a separate chemical compliance pathway.

Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.