Microwave Assisted Vacuum Dryer
Kerone’s Microwave Assisted Vacuum Dryer (MAVD) combines the penetrating volumetric heating power of microwave energy with the low-pressure, low-temperature benefits of vacuum processing to create one of the most effective drying solutions available to modern industry.
Engineered precision for Microwave Assisted Vacuum Dryer.
Kerone’s Microwave Assisted Vacuum Dryer (MAVD) combines the penetrating volumetric heating power of microwave energy with the low-pressure, low-temperature benefits of vacuum processing to create one of the most effective drying solutions available to modern industry.
At its core, the technology leverages the ability of microwave radiation to excite water molecules at the molecular level throughout the entire product mass simultaneously — in contrast to conventional surface-based heating methods that are inherently limited by conduction.
The vacuum environment lowers the boiling point of water to well below 100°C, enabling moisture evaporation at temperatures that are entirely safe for delicate biological, chemical, and food-grade materials. Together, these two mechanisms produce a dryer that is faster, gentler, and more energy-efficient than virtually any conventional alternative, making Kerone’s MAVD a transformative asset for quality-driven manufacturing operations.
Our advanced AI, ML, and IoT technologies, this solution delivers smarter automation, real-time insights, and predictive intelligence to enhance efficiency and drive future-ready growth.
Continuous tracking of process parameters with instant adjustments.
Intelligent fault detection to prevent failures before they occur.
Dynamic tuning of operations for maximum output and efficiency.
The thermodynamic architecture of our Microwave Assisted Vacuum Dryer incorporates advanced thermal modeling and computational fluid dynamics (CFD) to ensure optimal heat and mass transfer across the entire processing zone. By precisely controlling thermal gradients, air velocity profiles, and direct energy delivery mechanisms, the system achieves uniform treatment while preventing localized overheating, product degradation, or thermal stress. This balance of intensive heat transfer and controlled retention time ensures maximum operational throughput with minimal specific energy consumption.
Built with heavy-duty structural engineering and sanitary metallurgy, each unit is manufactured to withstand continuous 24/7 industrial operating conditions. Contact surfaces are finished in high-grade stainless steel (SS 304, SS 316L, or corrosion-resistant alloys) with sanitary mirror-polish options, CIP/SIP washdown provisions, and hermetic chamber sealing. This guarantees full compliance with stringent international hygiene, CE machinery directives, and cGMP standards across food, pharmaceutical, specialty chemical, and heavy manufacturing applications.
Proprietary control algorithms ensure strict process repeatability, while built-in safety interlocks and electromagnetic shielding comply with international CE and OSHA standards. Full process development support — including material loss tangent testing, moisture sorption isotherms, and pilot trials at our Ambernath R&D facility — ensures the selected technology matches your exact industrial throughput goals.
Product & Systems Gallery
Explore authentic high-resolution photographs of industrial machinery, pilot trial rigs, and continuous turnkey processing installations engineered by Kerone Engineering Solutions for Microwave Assisted Vacuum Dryer. Each system is fabricated at our ISO 9001:2015 certified manufacturing facilities with precision laser cutting, robotic welding, and stringent Factory Acceptance Testing (FAT).

Microwave Assisted Vacuum Dryer
Click to view high-res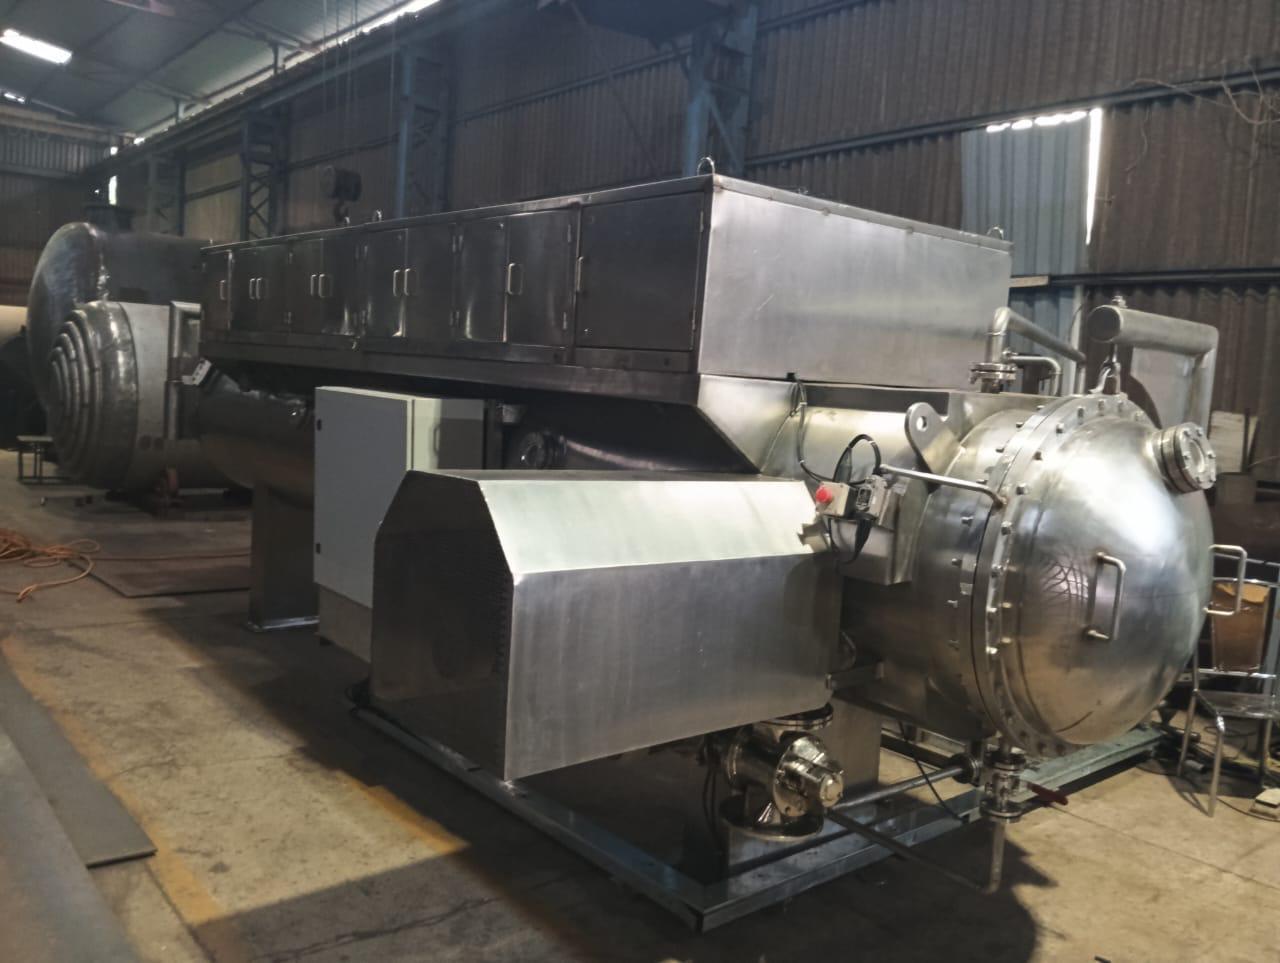
Microwave Assisted Vacuum Dryer
Click to view high-res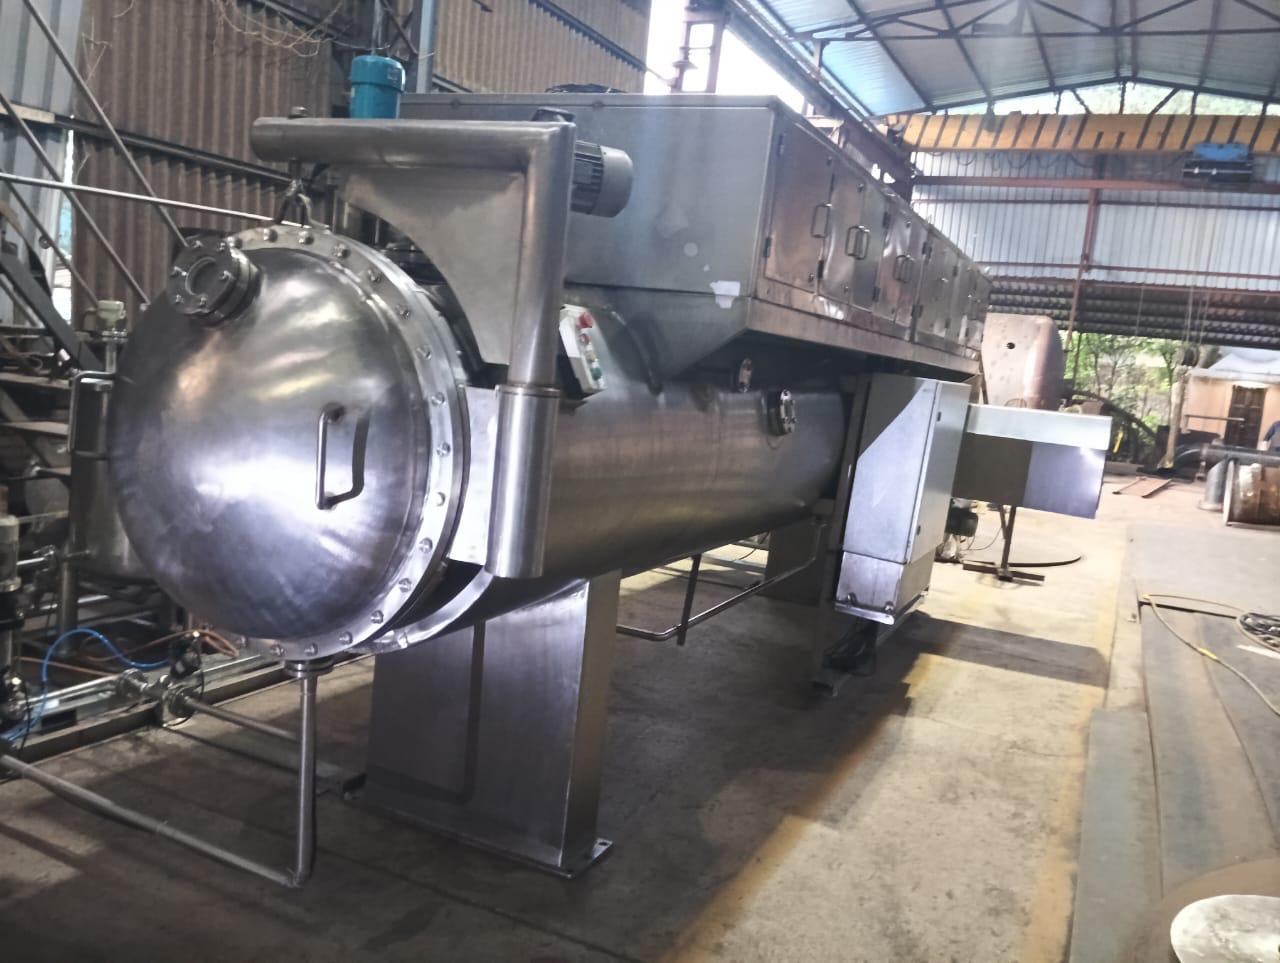
Microwave Assisted Vacuum Dryer
Click to view high-res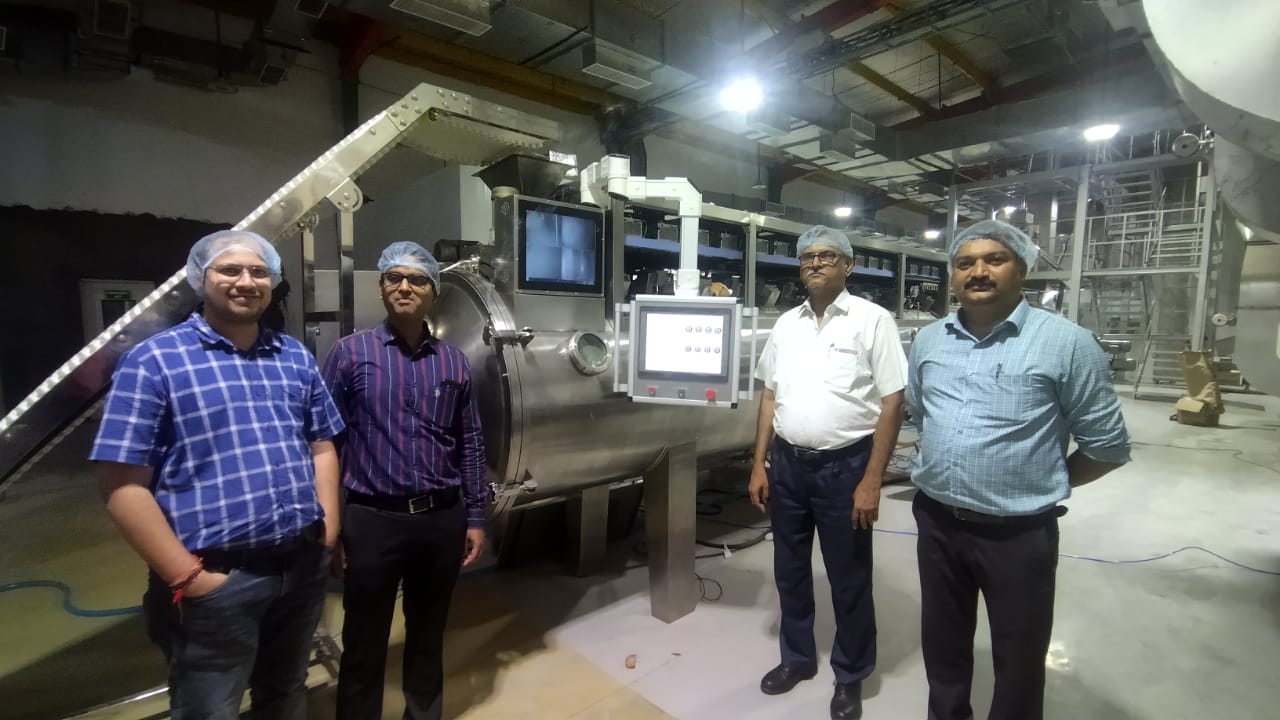
Microwave Assisted Vacuum Dryer
Click to view high-res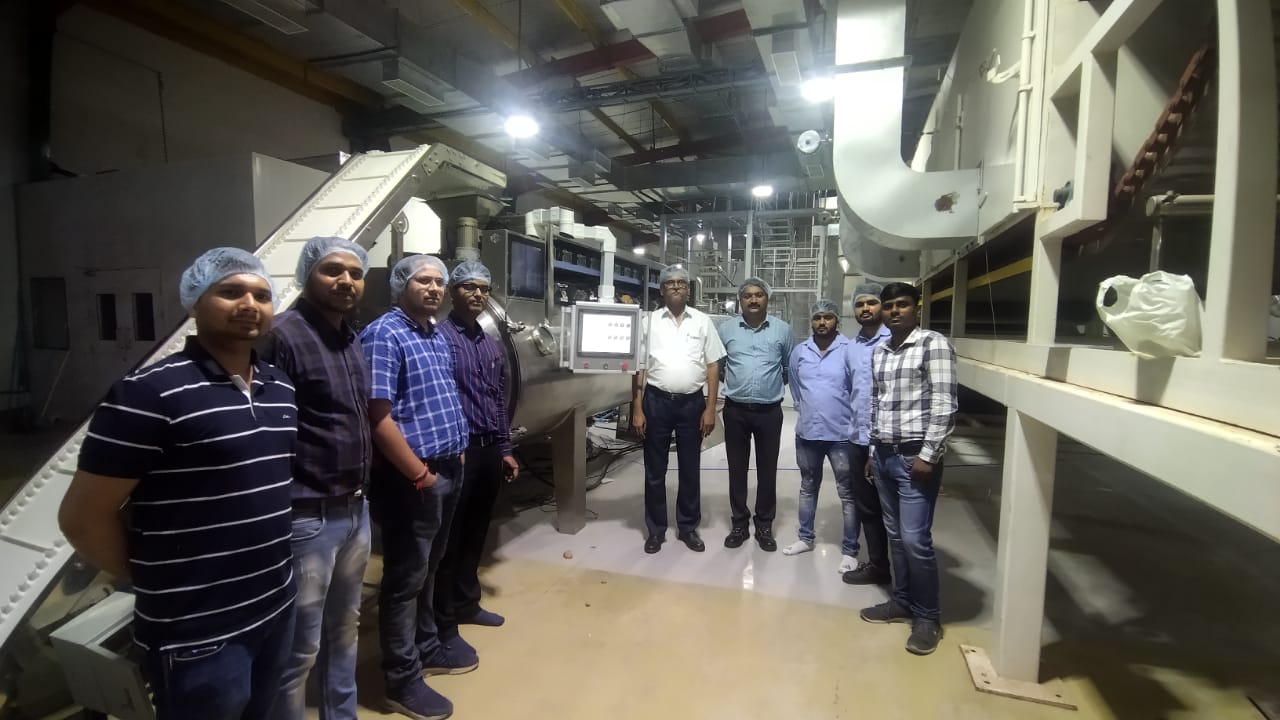
Microwave Assisted Vacuum Dryer
Click to view high-res
Microwave Assisted Vacuum Dryer
Click to view high-res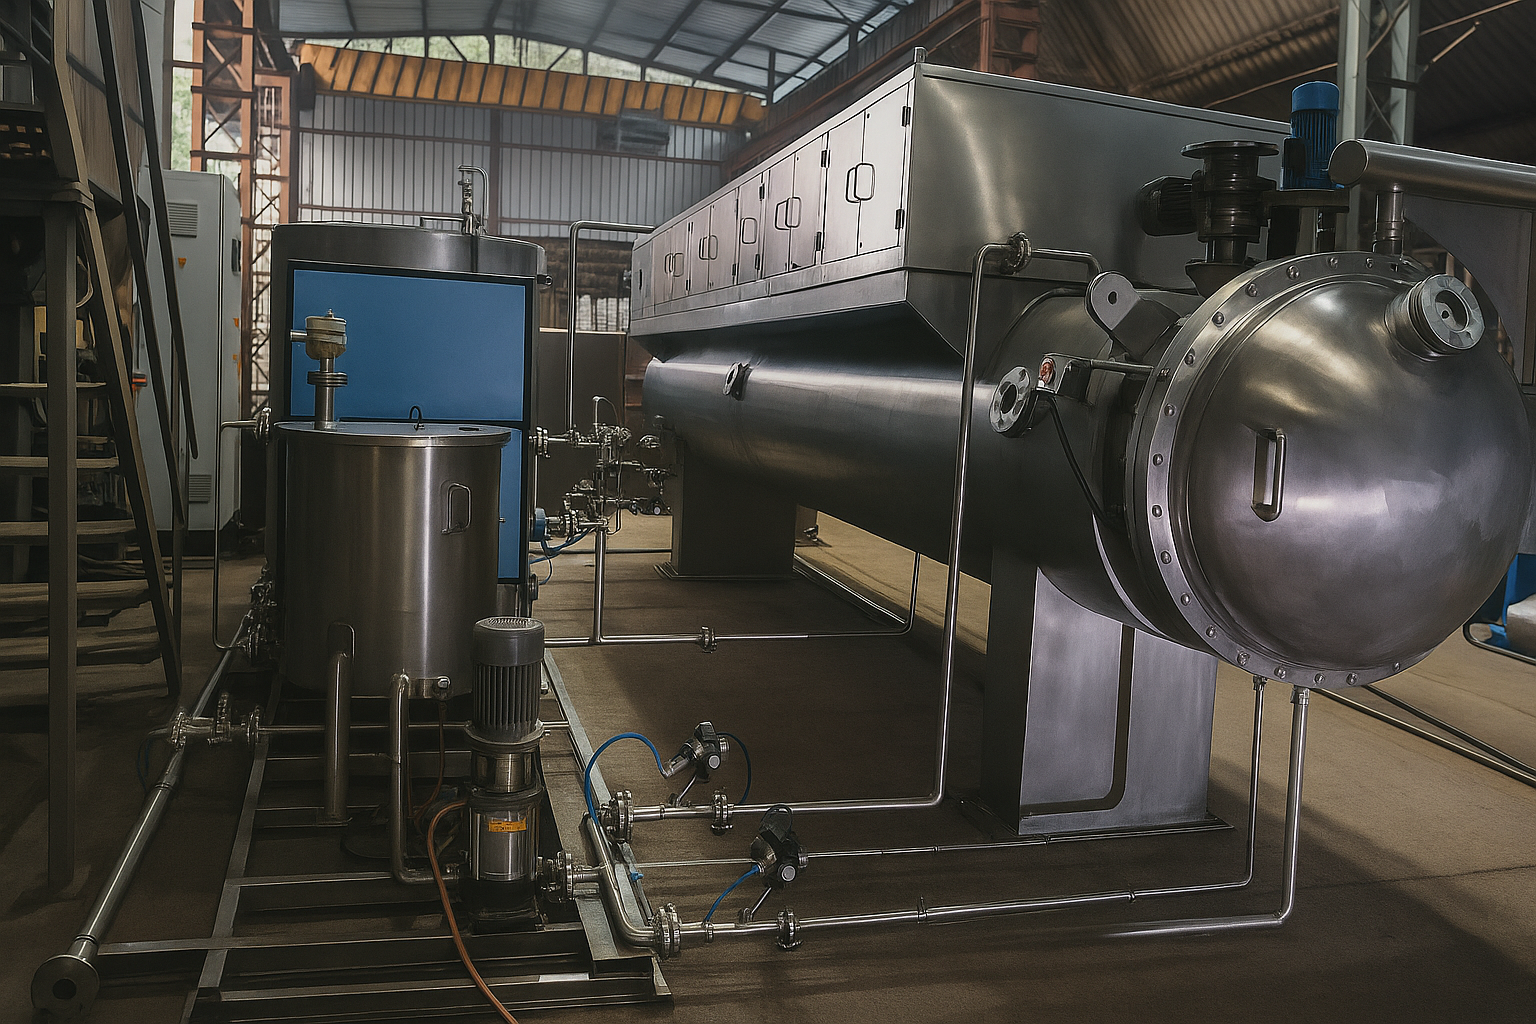
Microwave Assisted Vacuum Dryer
Click to view high-res50+ Years of Thermal Engineering Leadership.
Since 1976, Kerone Engineering Solutions has delivered over 5,000 custom-engineered thermal and process installations across 50+ countries. In technical collaboration with premier global institutions like CSIR-CEERI and University of Nottingham research partnerships, we design and manufacture high-efficiency machinery that minimizes production downtime and cuts operating expenses.
Unlike standard off-the-shelf equipment suppliers, Kerone operates a complete pilot-scale testing facility at our KRDC Ambernath center. We validate your exact raw material properties — determining moisture sorption isotherms, specific heat capacity, and dielectric behavior — before finalizing equipment sizing, ensuring zero risk during industrial scale-up.
Engineering precision, built into every system.
Simultaneous Microwave
Simultaneous microwave volumetric heating and vacuum moisture removal for drying speeds up to 10x faster than conventional tray drying
Adjustable Vacuum Levels From
Adjustable vacuum levels from 1,013 mbar (atmospheric) down to 10 mbar enabling customized low-temperature processing
Different Product Geometries
Choice of 2.45 GHz or 915 MHz microwave frequency to optimize energy penetration depth for different product geometries
Complex Drying Profiles
Multi-step programmable drying cycles with automatic power and vacuum level transitions for complex drying profiles
Easy Cleaning and Validation
Full stainless-steel construction with GMP-compliant smooth internal surfaces for easy cleaning and validation
Built-in Microwave Power
Built-in microwave power monitoring and reflected power protection ensuring operational safety and generator longevity
Compact, Space-efficient Footprint
Compact, space-efficient footprint with front-loading design for ergonomic product loading and unloading
Optional Inline NIR or Microwave
Optional inline NIR or microwave resonance moisture sensors for real-time endpoint determination and quality assurance
Powered by AI, Machine Learning & Smart IoT Integration
Modern industrial processing requires unprecedented thermal precision, energy efficiency, and operational agility. Kerone equips each system with high-speed industrial edge computing controllers, multi-spectral non-contact infrared pyrometry, and proprietary closed-loop machine learning algorithms that continuously analyze process parameters in real time.
The intelligent automation stack monitors dynamic changes in incoming material load, bed thickness, moisture content, and environmental factors. In response, our algorithms dynamically adjust heater power arrays, generator frequency, conveyor drive velocities, and exhaust dampers within milliseconds — entirely eliminating product burn, under-processing, or thermal hotspotting.
Seamlessly integrated with factory-wide SCADA and enterprise ERP architectures via native MQTT, OPC-UA, and Modbus TCP protocols, our systems deliver complete digital recipe control, remote diagnostics, predictive maintenance alerting, and tamper-evident batch logs compliant with global FDA 21 CFR Part 11 and cGMP standards.
Adaptive Heat Modulation
Neural algorithms detect material thermal variations in real time (<50ms response) and tune generator frequency and power arrays automatically.
IoT Cloud Telemetry
Continuous bidirectional telemetry stream via MQTT/OPC-UA protocols directly to centralized plant SCADA, MES, or mobile engineer dashboards.
Predictive Maintenance
Monitors magnetron cathode current, vibration frequency signatures, and differential filter pressure to schedule AMC maintenance before failures occur.
Quality & Batch Traceability
Automated digital recipe execution, multi-stage temperature ramp/soak curves, and cryptographically signed electronic batch logs compliant with 21 CFR Part 11.
Engineered for High-Value Industrial Sectors
Tailored thermal and process configurations across continuous manufacturing lines.
Herbal and botanical extract drying
preserving phytochemical potency, essential oils, and natural colors in plant: based materials
Food ingredient manufacturing
drying dairy powders, honey, fruit concentrates, and flavor compounds with full organoleptic retention
Chemical and polymer processing
drying hygroscopic specialty chemicals, resins, and polymer granules without oxidation
Agrochemical formulation
drying pesticide granules, water: dispersible powders, and microencapsulated active ingredients
Electronic component manufacturing
drying moisture: sensitive ceramic components, PCB laminates, and dielectric materials
Research and development
laboratory: scale process development and small: batch production of novel specialty materials
Configured to Your Process Window
Technical parameter envelopes across industrial manufacturing and engineering architectures.
Frequently Asked Questions
Engineering answers regarding equipment sizing, integration, and process performance.
Microwave energy penetrates the product and directly excites water molecules throughout the entire mass simultaneously, generating heat from within. This eliminates the surface-crust formation that impedes moisture migration in hot air drying, resulting in 5–10x faster and more uniform drying.
Materials that are heat-sensitive, high-value, or difficult to dry uniformly benefit most — including botanical extracts, pharmaceutical intermediates, food ingredients with high sugar content, and hygroscopic specialty chemicals.
The combined efficiency of microwave volumetric heating and vacuum moisture removal typically results in 40–70% lower energy consumption per kilogram of water removed compared to conventional hot air tray dryers.
Yes. Kerone offers rotary drum and agitated tray MAVD configurations specifically designed for processing liquid feeds, slurries, and paste-form materials into dried granules or powders.
Standard safety features include microwave leakage detection, reflected power shutdown, vacuum over-pressure relief valves, thermal runaway protection, interlocked door safety systems, and electrical surge protection.
The drying endpoint is determined by weight loss measurement, inline moisture sensors (NIR or microwave resonance), or time-based programs validated during Kerone's initial process development phase. Automated shutdown at target moisture content is standard.
Routine maintenance includes magnetron inspection every 2,000–5,000 hours, vacuum pump oil changes every 1,000 hours, door seal inspections quarterly, and annual full-system calibration, all supported by Kerone's service contracts.
Yes. Kerone offers ATEX-rated MAVD configurations with explosion-proof electrical enclosures, nitrogen-purged microwave entry systems, and integrated solvent recovery condensers for processing flammable or explosive materials.
Vacuum level selection is governed by the maximum temperature the product can tolerate without degrading, since lowering chamber pressure reduces water's boiling point and allows moisture to evaporate at a correspondingly lower temperature. A material that begins to degrade above 40°C, for example, would require a vacuum level deep enough to bring water's boiling point below that threshold, which typically means operating well below atmospheric pressure rather than at a shallow vacuum. Kerone's MAVD systems offer adjustable vacuum control down to 10 mbar specifically to accommodate this range of thermal sensitivity, with the exact operating point determined through process trials on the actual material.
Two main approaches are available: weight-loss monitoring, which tracks cumulative moisture removal against the batch's known starting weight, and spectroscopic moisture sensing using near-infrared (NIR) or microwave resonance technology, which measures moisture content directly without needing to interrupt the drying cycle. NIR sensing works well for materials with consistent optical properties, while microwave resonance sensing can be advantageous because it uses the same underlying physics as the drying process itself. Many production systems combine both approaches, using weight loss as a primary trend indicator and spectroscopic sensing to confirm the precise endpoint before automatically triggering cycle completion.
Freeze-drying achieves excellent product quality preservation but requires long cycle times, often spanning many hours to days, along with energy-intensive refrigeration to maintain the frozen state throughout primary and secondary drying. Microwave vacuum drying can achieve comparably low processing temperatures without the freezing step, often completing in a fraction of the time freeze-drying requires, which translates into significantly higher throughput per unit of equipment and lower energy cost per batch. The trade-off is that not every product responds identically to the two methods, so materials with very specific structural requirements, such as certain biologics needing the exact cellular matrix preservation freeze-drying provides, may still require freeze-drying despite the speed advantage of microwave vacuum processing.
Ongoing costs break down into electricity consumption for the microwave generators and vacuum pumps, scheduled maintenance covering magnetron and pump servicing, and consumables such as vacuum pump oil and door seal replacement. Because microwave vacuum drying typically reduces energy consumption substantially compared to conventional hot air drying for the same moisture removal task, the electricity line item is often lower than facilities initially expect when transitioning from older drying technology. Maintenance costs are relatively predictable since they follow defined service intervals rather than unplanned breakdowns, making total operating cost reasonably straightforward to forecast once a facility has baseline throughput and utility rate data.
ATEX-rated configurations address flammability risk through several integrated design elements: explosion-proof electrical enclosures prevent ignition sources from contacting flammable vapors, nitrogen purging of the microwave entry points displaces oxygen in zones where sparking could otherwise occur, and integrated condensers recover evaporated solvent rather than allowing it to accumulate as vapor within the drying chamber. Vacuum operation itself also reduces fire risk somewhat by limiting available oxygen, though this alone is not sufficient without the additional explosion-proofing measures. Facilities processing solvent-containing materials should specify ATEX requirements at the outset, since retrofitting explosion protection onto a standard system afterward is far more costly than building it in from the start.
Because microwave vacuum drying removes moisture quickly at low temperature, it tends to better preserve the cellular structure of the original material compared to slow, high-temperature drying methods that can cause cell wall collapse and case hardening. This structural preservation often translates into improved rehydration characteristics, since a less collapsed internal structure rehydrates more readily and completely than a densely shrunken one. For botanical extracts specifically, the lower processing temperature and shorter exposure time also help retain volatile aromatic compounds and heat-sensitive phytochemicals that would otherwise degrade or evaporate under prolonged conventional drying conditions.

Let’s Engineer the Right Process.
From application trials to full-scale production systems, our engineering team works with you to develop the right thermal processing solution for your material, throughput, and production requirements.